Formula details
Product Details
Overview
What Makes a Durable Sharp Iron Slitter Blade?
Delivering continuous, high-speed slitting without edge degradation requires a precise balance of metallurgy, thermal processing, and micro-inch machining.
Key Metallurgical Compositions
Selecting the right grade ensures our rotary slitter knives resist abrasive wear and shock impact during continuous coil processing:
| Tool Material | Hardness Range | Key Characteristic | Best Suited For |
|---|---|---|---|
| D2 Tool Steel | 58–62 HRC | High carbon/chromium wear resistance | Standard cold-rolled and hot-rolled iron slitting |
| High-Speed Steel (M2/M42) | 62–66 HRC | Superior red-hardness and edge toughness | High-speed, continuous coil slitting lines |
| Tungsten Carbide | 88–92 HRA | Extreme compressive strength & longevity | Thin-gauge, ultra-high-volume iron strip processing |
Vacuum Heat Treatment and Cryogenic Processing
Edge retention begins with structural stability. We utilize a multi-stage thermal cycle to harden each blade evenly from core to edge:
- Vacuum Hardening: Prevents surface decarburization and oxidation, ensuring uniform grain structure throughout the tool body.
- Deep Cryogenic Treatment (-300°F): Converts residual austenite into stable martensite, dramatically improving wear resistance and micro-chipping resistance.
- Triple-Cycle Tempering: Relieves internal stress, preventing blade fracture under severe radial and axial cutting loads.
Mirror-Finish Surface Grinding
Surface friction accelerates tool wear and degrades cut quality. Our metal coil slitting blades undergo ultra-fine surface lapping and polishing:
- Surface Roughness (Ra < 0.1 µm): Achieves a mirror-like finish that eliminates micro-frictional drag.
- Anti-Galling Performance: Prevents iron dust, coatings, and scale buildup along the cutting edges.
- Cleaner Shear Transitions: Reduces edge friction to ensure smooth strip separation without edge welding.
Precision Tolerance Standards
To eliminate burrs and slitting variations, we manufacture every rotary shear disc to uncompromising machine tolerances:
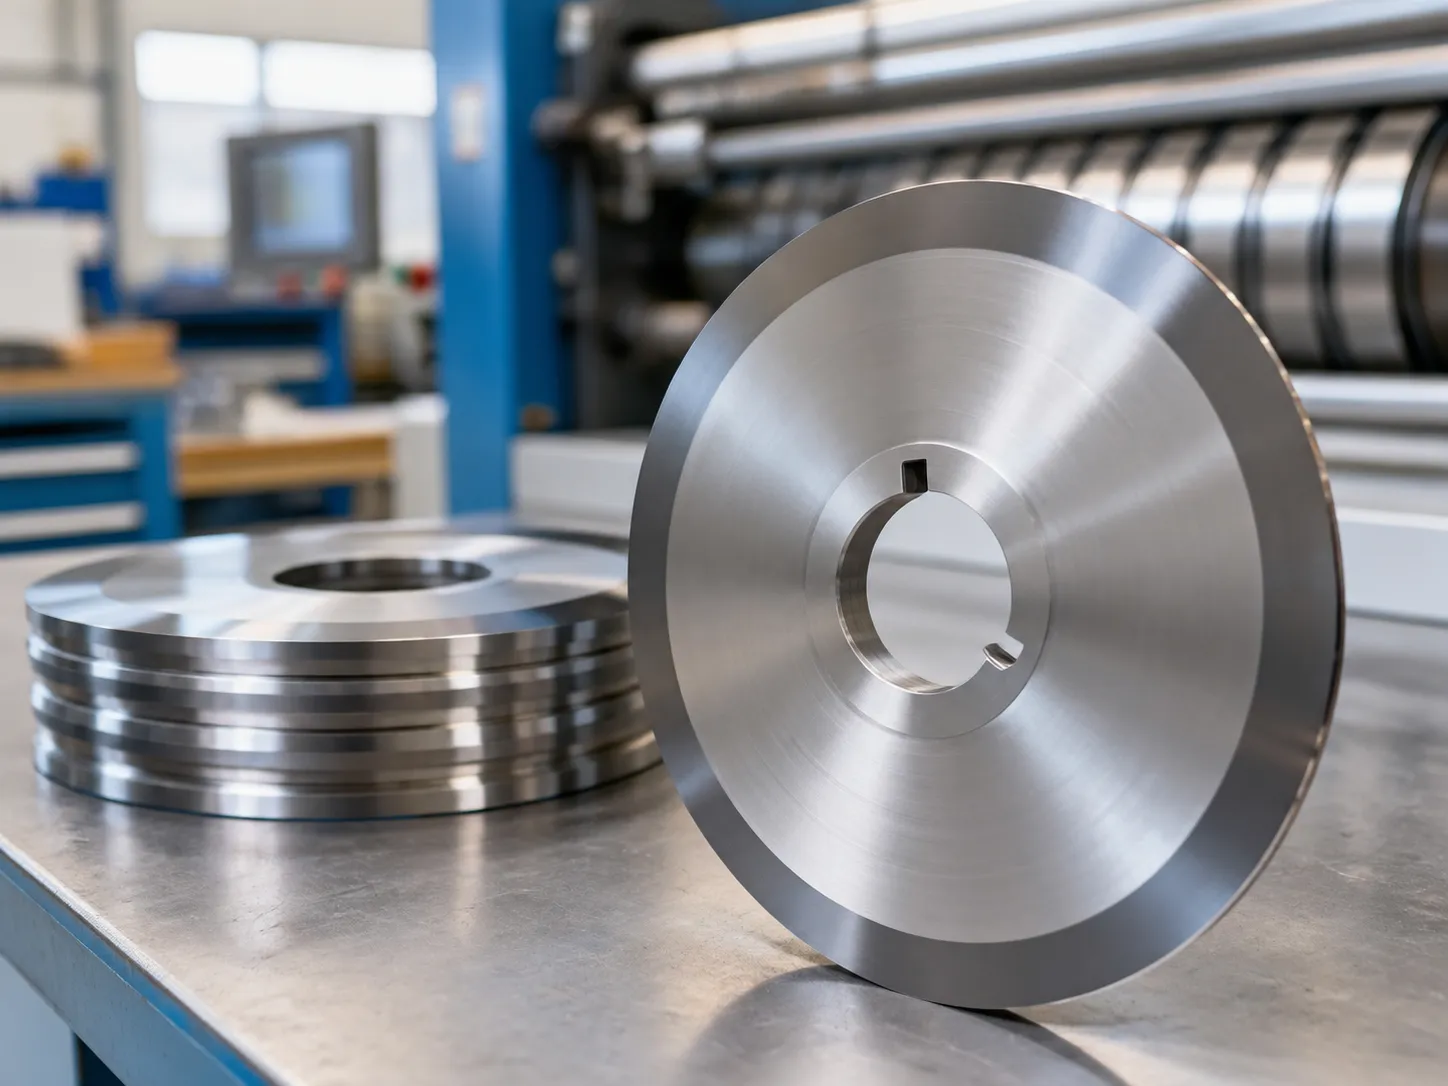
- Thickness Tolerance: Controlled within ±0.001 mm (±0.00004") to guarantee exact horizontal knife clearance across complex arbor setups.
- Flatness & Parallelism: Held within 0.002 mm (0.00008") to prevent blade wobble, side deflection, and uneven knife overlap.
- Bore Concentricity: Precision ground to eliminate arbor runout, reduce vibration, and extend machine bearing lifespan.
Key Performance Advantages in Metal Coil Slitting
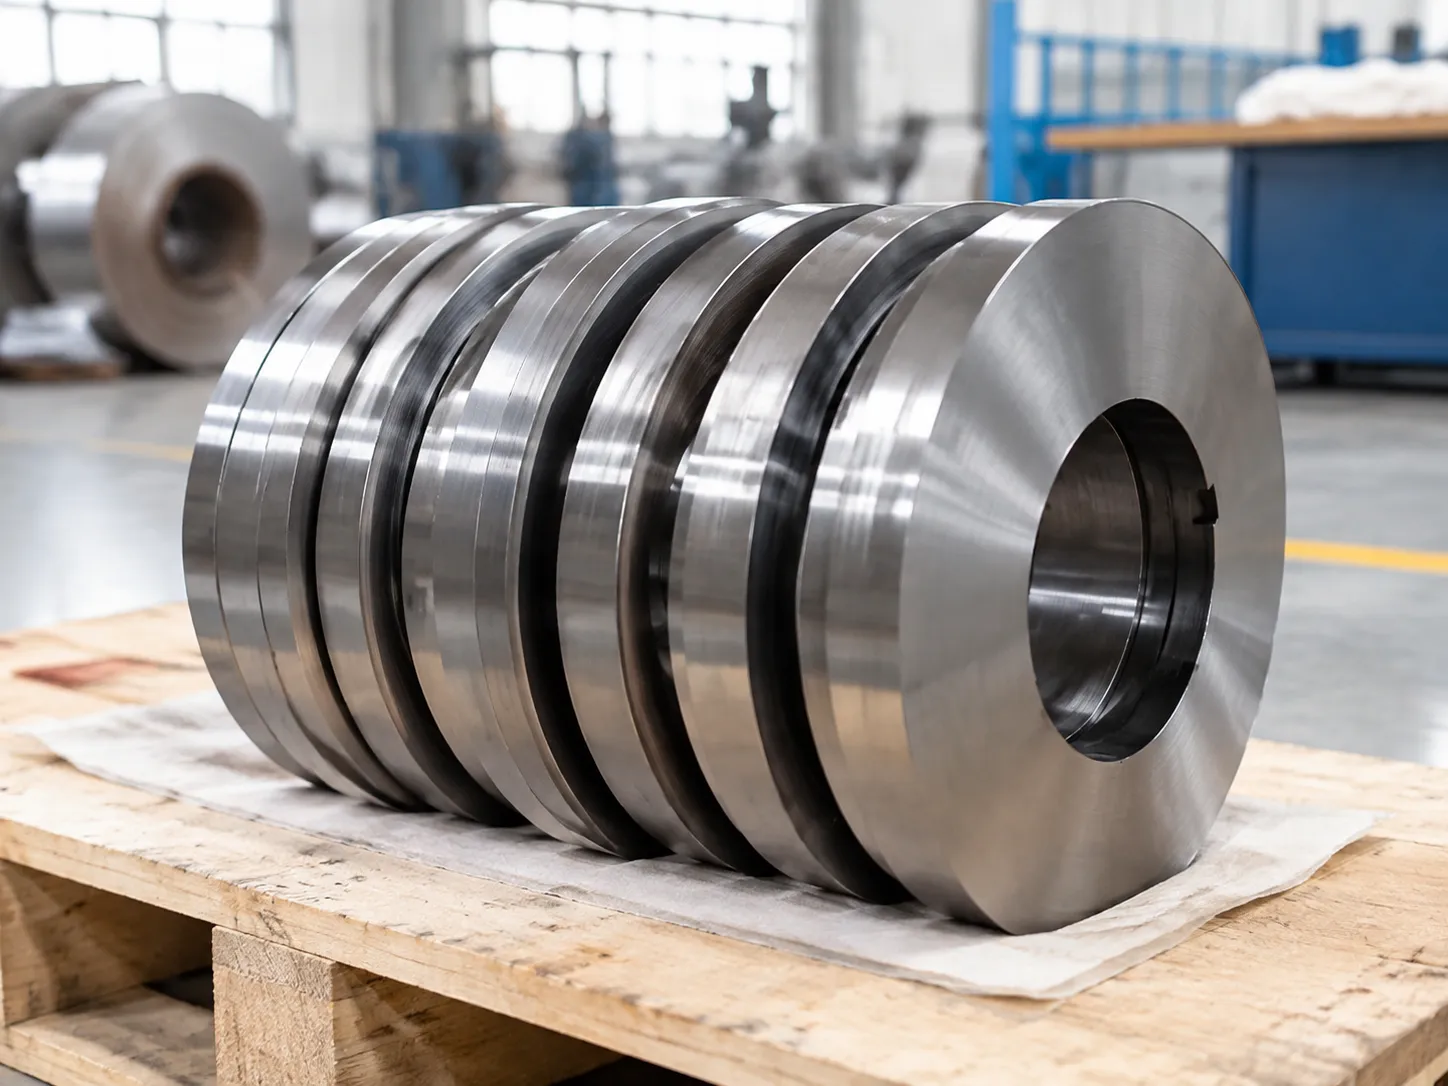
Consistent Burr-Free Slitting on Iron and Steel Coils
A razor-sharp, properly seated blade produces a clean shear-to-break ratio across the entire strip width. By maintaining razor-sharp cutting geometry, our blades eliminate edge camber, rollover, and heavy burrs on both ductile iron and high-strength steels. Understanding how rotary knife cutters work in metal slitting makes it clear: absolute edge sharpness eliminates strip deformities and delivers flat, ready-to-weld strip edges every time.
Resistance to Chipping, Spalling, and Premature Wear
Processing unpickled hot-rolled surfaces and abrasive scale easily ruins lower-grade knives. Our metal coil slitting blades deliver maximum toughness:
Microstructure Toughness: Advanced core metallurgy stops edge fracture and micro-chipping under sudden shock loads.
Flank Wear Resistance: Side-faces resist frictional scouring from tightly clamped strips.
Spall Prevention: Uniform heat treatment prevents surface layers from flaking away along the outer diameter.
Reduced Machine Downtime and Longer Regrind Intervals
Frequent tooling changes quickly destroy operating margins. Because these high wear resistance blades hold their cutting edge through hundreds of tons of continuous coil, your setup crews spend less time tearing down arbors. Fewer blade swaps lead directly to:
Extended running cycles between scheduled regrinds
Minimized arbor repositioning and shim adjustments
Lower annual tooling expenditures and reduced regrinding scrap
High-Speed Operational Stability Under Continuous Load
At high line speeds, any imbalance or runout leads to chatter marks and knife rubbing. Our rotary slitter knives maintain structural rigidity and thermal stability under continuous production schedules. The blades resist deflection and heat expansion across the arbor, ensuring uniform clearance and tight slit-width tolerances from the master coil's head to its tail.
Common Industrial Applications of Durable Sharp Iron Slitter Blades
Our durable sharp iron slitter blades are engineered to handle the toughest coil processing environments across global manufacturing sectors. Designed for high wear resistance and structural integrity, these blades deliver clean, predictable shearing across a wide range of ferrous materials and specialized alloys. We match blade geometry and metallurgy directly to your slitting line requirements, ensuring consistent performance across all major industrial applications.
- Hot-Rolled and Cold-Rolled Iron Sheet Slitting: Hot-rolled coils carry tough mill scale that wears down inferior tooling quickly. Our blades resist abrasive wear during primary breakdown slitting. For cold-rolled iron and sheet stock, our high-precision sheet metal slitter knives maintain tight dimensional tolerances and crisp edges without edge roll-over.
- Galvanized, Silicon, and Electrical Steel Processing: Coated and electrical steels require razor-sharp cutting edges to prevent zinc flaking, coating damage, and edge-induced magnetic loss. Our tooling guarantees burr-free cuts on grain-oriented and non-oriented electrical steel coils.
- Automotive Chassis and Stamping Coil Preparation: Advanced high-strength steels (AHSS) and structural iron coils used in automotive stamping demand extreme edge toughness. Our rotary slitter knives eliminate micro-fractures on slit strip edges, preventing splitting during downstream stamping and deep drawing.
- Heavy-Duty Tube and Pipe Mill Entry Lines: Tube and pipe production requires heavy-gauge slit coils with square, uniform edges to ensure flawless seam welding. Our heavy-duty slitter knives process thick-gauge iron coils continuously without chipping or edge deflection under high shear loads.
Compatible Materials Breakdown
| Material Type | Typical Thickness Range | Processing Objective | Recommended Blade Feature |
|---|---|---|---|
| Hot-Rolled Iron / Carbon Steel | 1.5 mm – 16.0 mm | Heavy-gauge slitting, scale tolerance | Shock-resistant D2 / Modified tool steel |
| Cold-Rolled Iron & Steel | 0.2 mm – 3.2 mm | Precision width control, burr-free edges | High-Speed Steel (HSS) with mirror finish |
| Galvanized / Coated Sheet | 0.4 mm – 2.5 mm | Zero zinc spangle peeling, clean separation | Tungsten carbide or ultra-fine grain tool steel |
| Silicon / Electrical Steel | 0.15 mm – 0.65 mm | Low core-loss edge retention, ultra-tight gap | Precision-ground sub-micron carbide discs |
Proper Blade Setup and Clearance for Maximum Sharpness
Calculating Horizontal and Vertical Knife Clearance
Knife clearance directly dictates cut quality, burr height, and edge longevity. Getting the right gap between your upper and lower rotary slitter knives requires balancing horizontal clearance (gap) and vertical clearance (overlap):
- Horizontal clearance: For standard mild iron, set side clearance to roughly 7% to 10% of material thickness. Higher-strength iron or heavier gauges typically need 10% to 14% to ensure a clean fracture zone without tearing.
- Vertical clearance (penetration): Thin sheet metal requires slight knife penetration (overlap), while heavy-gauge coils require positive clearance (an open vertical gap) to allow the iron sheet to shear naturally rather than pinch.
- The golden ratio: Aim for a clean 25–35% cut band and a uniform break zone across the entire coil width.
Arbor Alignment, Backlash Control, and Runout Minimization
Maintaining strict arbor runout tolerance is vital for uniform edge engagement. Axial and radial runout should never exceed 0.005 mm (0.0002 inches) on precision slitting lines:
- Eliminate arbor deflection: Check your arbor bearings regularly. Any play or wobble magnifies tool wear and chips razor edges under load.
- Lock down backlash: Excessive gear play allows knives to stutter upon entry, which fractures the cutting edge of a high-hardness sheet metal slitter knife.
- Parallel arbors: Keep upper and lower arbors strictly parallel under full clamping pressure to prevent uneven depth of cut from drive-side to operator-side.
Selecting Matched Stripper Rings, Spacers, and Shims
Your supporting tooling holds the slitting setup rigid and controls coil tracking:
| Tooling Component | Selection Rule | Function |
|---|---|---|
| Precision Spacers | Hardened tool steel, ground parallel within ±0.002 mm | Locks knife position across the arbor width |
| Micro-Shims | Color-coded stainless steel or brass | Provides fine-tuned knife clearance calculation adjustments |
| Stripper Rings | Shore A durometer matched to gauge (70–90A) | Supports strip eject, dampens chatter, and prevents distortion |
Much like setting up an ultra-precise foil slitter blade line, your spacer faces and blade contact surfaces must be kept spotless. Any dirt, oil film, or burrs between spacers will cause cumulative runout across the arbor.
Preventing Side-Load Stress and Edge Contact Damage
Physical contact between upper and lower slitter blades instantly dulls or fractures sharp cutting edges. We prevent catastrophic edge failure with these operational rules:
- Never allow zero clearance: Steel and iron coils push back against blade faces. A setup with insufficient horizontal clearance will deflect knives into one another under load.
- Control strip camber: Severe coil camber creates intense lateral thrust against the blade sidewalls, leading to friction burn and chipped rims.
- Check locknut torque: Apply calibrated hydraulic or spanner torque evenly across arbor locknuts to avoid tilting spacers and pinching our industrial slitting blades.
Maintenance, Regrinding, and Storage Best Practices for Durable Sharp Iron Slitter Blades
Routine care keeps every durable sharp iron slitter blade running at peak performance. Implementing proven knife maintenance best practices protects your tooling investment, minimizes line downtime, and maintains tight slit-edge tolerances on every iron coil run.
Visual Inspection Markers for Blade Wear
We recommend checking rotary shear knives during every setup changeover. Catching early wear indicators prevents catastrophic edge chipping:
- Dulling and Edge Radiusing: Rounded cutting edges show light reflection along the perimeter, signaling it is time for a regrind.
- Micro-Cracks and Micro-Chipping: Tiny fractures along the shear face caused by excessive side loads or foreign material.
- Wear Tracks and Galling: Vertical rub marks and material pickup across the blade faces, indicating improper stripper ring pressure or clearance misalignment.
| Inspection Item | Warning Signs | Action Required |
|---|---|---|
| Cutting Edge | Light reflection, micro-chips | Schedule precision regrind |
| Side Faces | Galling, deep score marks | Clean, lap, and check clearance |
| Bore / Arbor Fit | Fretting corrosion, burrs | Polish bore and check arbor runout |
Precision CNC Resharpening Parameters
Proper slitter blade regrinding restores cutting geometry without reducing blade lifespan unnecessarily:
- Minimum Stock Removal: Remove only 0.02 mm to 0.05 mm (0.001" to 0.002") per pass using flood coolant to prevent thermal shock and micro-cracking.
- Surface Finish: Polish grinding surfaces to a mirror finish (Ra < 0.2 µm) to eliminate friction and resist metal pickup.
- Parallelism and Flatness: Maintain face parallelism within 0.002 mm to prevent blade wobble and edge contact during high-speed iron slitting.
Safe Handling and Storage Organization
Protecting razor-sharp cutting edges between production runs is vital for workplace safety and tooling longevity:
- Protective Edge Guards: Always transport and mount rotary slitter knives with heavy-duty rubber or polymer edge protectors.
- Anti-Corrosion Application: Coat clean, dry blades with industrial-grade rust-preventative oil before long-term storage.
- Dedicated Storage Racks: Store knives horizontally on wooden or polyurethane-lined arbor pins with non-abrasive spacers to prevent direct steel-on-steel contact.
How to Choose the Right Slitter Blade for Your Slitting Line
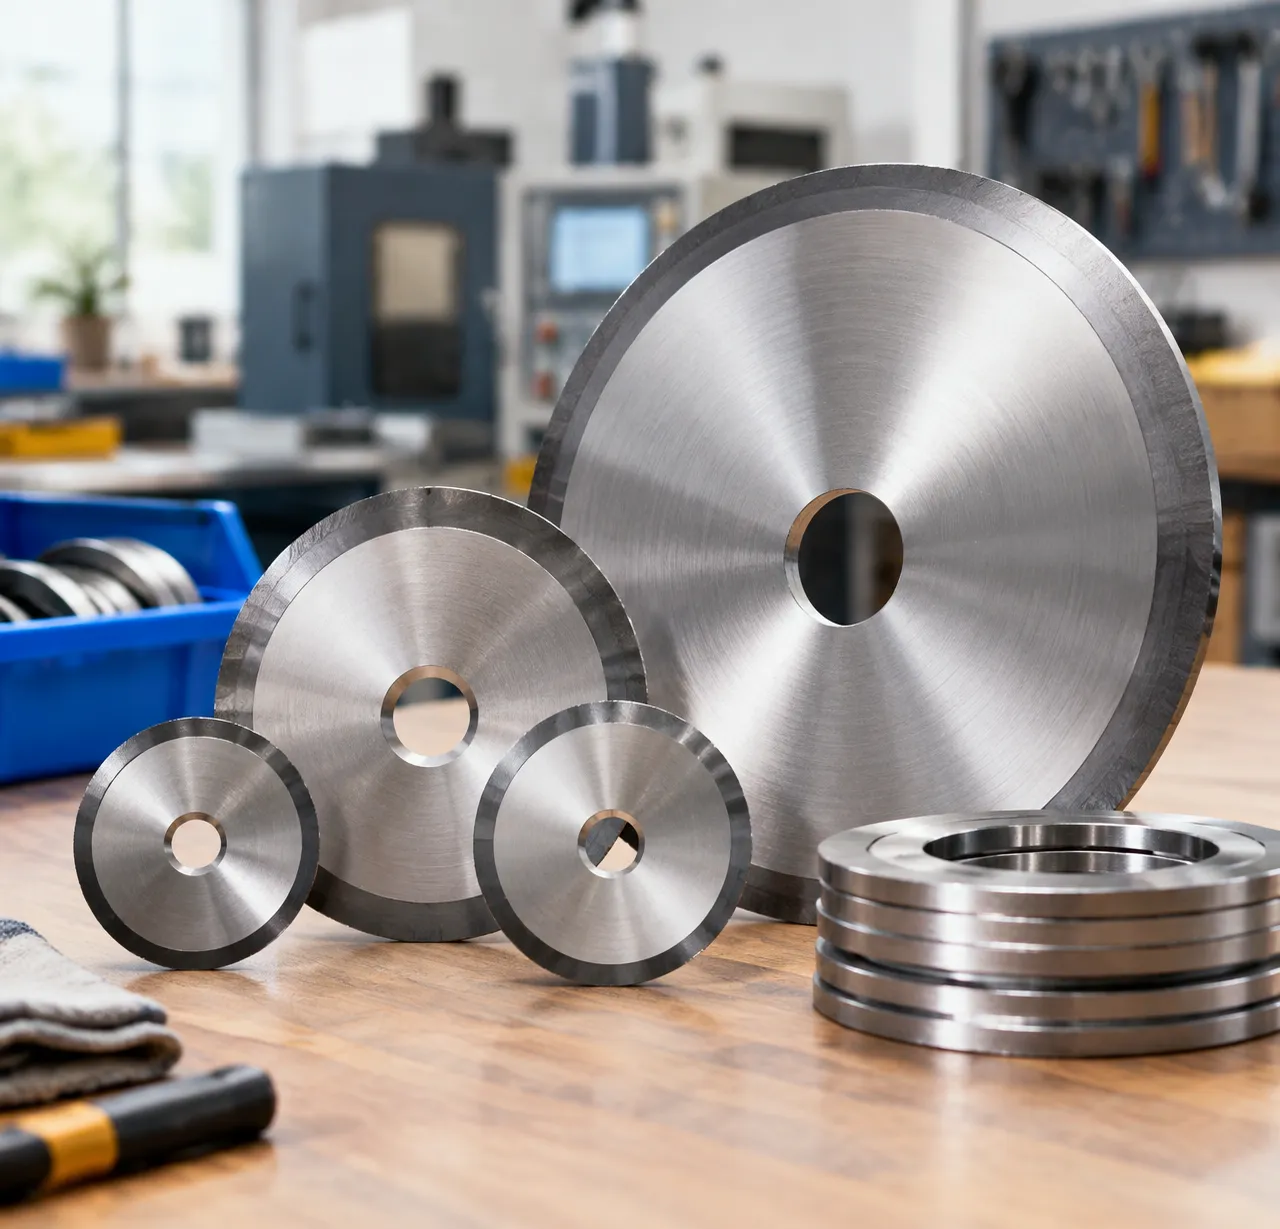
Selecting the ideal durable sharp iron slitter blade depends on matching your coil metallurgy with precise tooling geometry.
Matching Blade Hardness (HRC) to Coil Tensile Strength
Tool hardness must counterbalance coil strength to prevent chipping or rapid dulling. For comprehensive tooling strategies, check our guide on how to choose slitting knives across various steel grades.
| Coil Material & Tensile Strength | Recommended Blade Material | Target Hardness (HRC) | Key Performance Advantage |
|---|---|---|---|
| Low-Carbon Iron (< 450 MPa) | D2 Tool Steel / High-Speed Steel | 58–60 HRC | Excellent balance of wear resistance and toughness |
| Medium Tensile / Galvanized (450–700 MPa) | Premium D2 / High-Carbon Alloy | 60–62 HRC | High edge sharpness with reduced galling risk |
| High-Strength / Electrical Steel (> 700 MPa) | Tungsten Carbide / M2 HSS | 62–65 HRC | Maximum wear resistance under severe side load |
Outer Diameter (OD), Inner Diameter (ID), and Thickness Sizing Guide
To maintain cutting precision and eliminate arbor deflection, our rotary slitter knives adhere to strict dimensional sizing:
- Outer Diameter (OD): Sized to provide sufficient overlap without excessive peripheral speed variance.
- Inner Diameter (ID): Precision-ground to match arbor diameters within tight tolerances (H3 to H5 fit) to eliminate runout.
- Blade Thickness: Thicker bodies provide stability on heavy-gauge coils, while ultra-thin profiles minimize material waste on light-gauge strip iron.
Single-Edge vs. Double-Edge Rotary Knife Configurations
- Single-Edge Blades: Ideal for dedicated slitting setups. The flat side delivers stable side-clearance support, making it standard for high-tonnage heavy-duty coil lines.
- Double-Edge Blades: Feature cutting edges on both sides. Once one side wears down, simply flip the blade to double your working time before sending it out for regrinding.
Custom OEM Specifications vs. Standard Off-the-Shelf Tooling
- Standard Off-the-Shelf Tooling: Readily available for standard arbor shafts, offering fast replacement times for common iron and sheet metal slitting tasks.
- Custom OEM Tooling: Engineered with tailored keyways, specialized cryogenic treatments, and matched stripper rings to fit non-standard coil processing equipment and automated high-speed slitting lines.
Frequently Asked Questions About Iron Slitter Blades
How long does a sharp iron slitter blade typically last before regrinding?
A high-performance durable sharp iron slitter blade made from premium tool steels like D2 or high-speed steel typically processes 150 to 300 tons of standard iron coil before requiring maintenance. Service life varies based on coil thickness, tensile strength, and line speed. Tooling made from tungsten carbide can last up to 5 to 10 times longer on continuous thin-gauge lines when operated under proper arbor alignment.
What causes burrs on the slit edge of iron sheets?
Edge burrs occur when the cutting dynamics shift from clean shearing to tearing. Common culprits include:
- Excessive horizontal clearance: The gap between the upper and lower knives is too wide.
- Dull cutting edges: Micro-chipping or rounded edges fail to fracture the metal cleanly.
- Arbor deflection or runout: Shaft vibration alters knife spacing during continuous high-speed runs.
- Improper vertical overlap: Knives penetrate either too deep or too shallow into the iron strip.
Can I use carbide slitter blades for heavy-gauge iron coils?
We do not recommend solid tungsten carbide blades for heavy-gauge iron coils (generally over 3.0 mm) or hot-rolled metals with heavy scale. Carbide provides unmatched wear resistance but lacks the impact toughness needed for heavy-duty shock loads. For heavy-gauge coil slitting, shock-resistant tool steels like D2 or modified H13 provide the ideal balance of toughness and edge stability. For medium-gauge slitting setups, using standard circular tooling like a 170mm slitter blade ensures high fracture toughness without chipping.
How much material should be ground off during blade resharpening?
Precision regrinding should remove only the damaged shear zone—typically between 0.02 mm and 0.05 mm (0.0008" to 0.002") per pass using flooded coolant to prevent thermal stress. For scheduled maintenance before severe edge breakdown occurs, standard precision slitter blades require removing as little as 0.01 mm to 0.03 mm to restore a clean, mirror-finished cutting radius.
What is the ideal clearance tolerance for iron coil slitting?
Optimal clearance depends on metal thickness and tensile grade:
- Horizontal clearance: Set between 7% and 12% of strip thickness for soft to medium iron sheet, and up to 15% to 18% for high-strength steel.
- Vertical penetration (overlap): Typically set between -0.5 mm to +1.0 mm, depending on coil thickness (thicker gauges require positive clearance/gapping, while thin foils require slight overlap).