Formula details
Product Details
Overview
Technical Specifications and Material Selection Guide
Key Dimensional Parameters
Our manufacturing process accommodates both standard OEM dimensions and custom size-reduction setups:
- Outer Diameter (OD): Sized to match rotor swing radiuses and chamber depths for optimized hook penetration.
- Blade Thickness: Precision-ground faces ensure tight lateral stacking, maintaining accurate axial clearance and zero blade-to-blade play.
- Bore Profiles: Custom-machined to match drive system torque requirements, including:
- Hexagonal bores for balanced torque distribution
- Splined shafts for high-load industrial applications
- Square bores and round bores with single or double keyways
- Machining Tolerances: Precision CNC milling and grinding down to ±0.01 mm to ±0.005 mm for seamless interlocking.
Tool Steel and Alloy Performance Matrix
We match raw steel grades to your specific processed waste stream to achieve the ideal balance between hardness, wear resistance, and impact toughness.
| Steel Grade | Hardness (HRC) | Primary Mechanical Characteristics | Recommended Shredding Applications |
|---|---|---|---|
| D2 (1.2379 / SKD-11) | 58–62 HRC | High carbon, high chromium; exceptional abrasive wear resistance | Rigid plastics, PET bottles, films, packaging waste |
| DC53 | 58–62 HRC | Improved toughness over D2; excellent fatigue strength and edge retention | Mixed plastics with minor contaminants, electronics, cables |
| Cr12MoV | 56–60 HRC | Reliable wear resistance with good thermal stability | General industrial waste, municipal solid waste (MSW) |
| 55SiCr / 6CrW2Si | 54–58 HRC | Superior shock resistance; resists cracking under sudden shock loads | High-impact scrap metal shearing, light metal turnings |
| H13 (1.2344) | 52–56 HRC | High hot-work toughness and resistance to thermal fatigue | Bulky timber, heavy-duty e-waste, continuous high-friction shredding |
| Hardox / Overlays | 50–55 HRC | High structural toughness with optional wear-resistant surface facing | End-of-life tires (ELT), contaminated scrap, heavy construction debris |
Severe-Duty Impact Alloys and Hardox Overlays
For applications subjected to uncrushable tramp materials or severe abrasive wear, standard tool steels may suffer from catastrophic cracking. In these operating environments, we utilize:
- Shock-Resistant Structural Alloys (55SiCr, 6CrW2Si, 42CrMo): Tempered specifically to absorb continuous high-impact energy without tooth fracture.
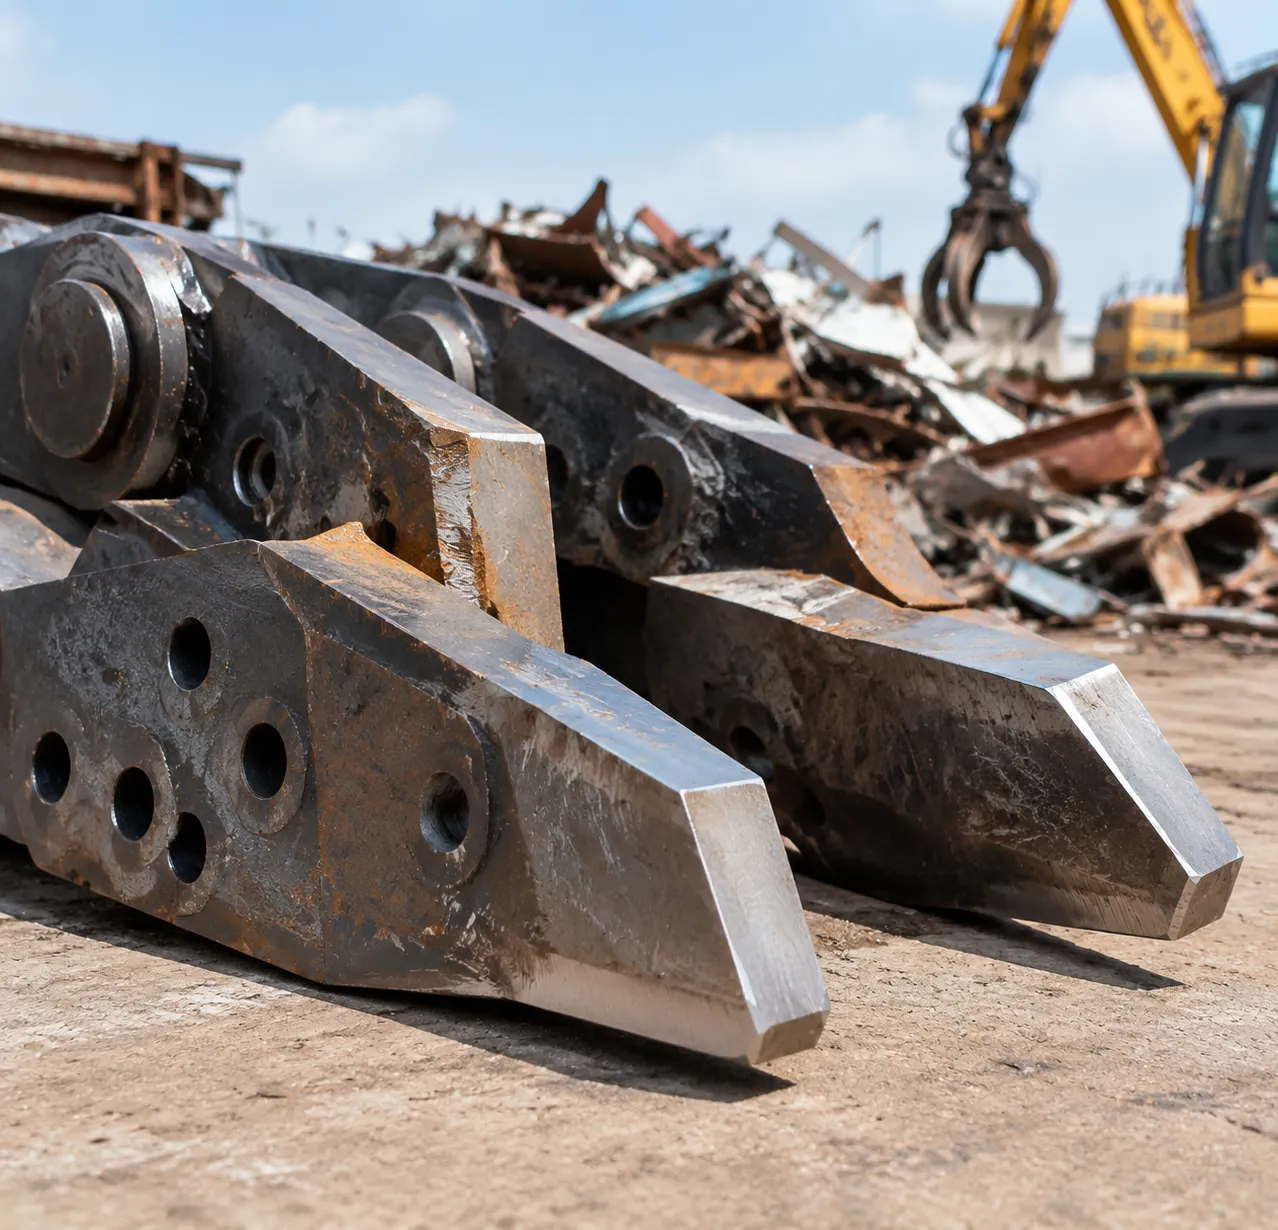
- Hardox Wear Plates & Reinforced Overlays: Tough core structures combined with hardfacing options provide reliable tearing action for bulky industrial refuse, scrap rubber, and whole tires.
Proprietary Heat Treatment and CNC Manufacturing Process
Achieving maximum wear life and impact resistance in double shaft shredder blades comes down to controlled thermal processing and high-precision machining.
Multi-Stage Vacuum Furnace Heat Treatment
Standard atmosphere heating can cause surface decarburization, leading to soft edges and premature wear. We utilize multi-stage vacuum heat treatment furnaces with high-pressure nitrogen quenching:
Uniform Core Toughness: Prevents catastrophic blade snapping when uncrushables enter the cutting chamber.
Controlled Hardness Gradient: Delivers structural hardness calibrated between 54 to 62 HRC depending on your target waste stream and steel selection.
Zero Decarburization: Preserves the metallurgical integrity of high-alloy tool steels during thermal cycles.
Triple Cryogenic Sub-Zero Tempering
To eliminate retained austenite and relieve internal stresses, our blades undergo deep cryogenic sub-zero treatment followed by triple tempering cycles. This specialized process stabilizes the steel microstructure, significantly improving edge stability under high-torque shearing. You can explore how we optimize these parameters in our detailed guide on D2 steel heat treatment.
Precision CNC Machining & Tight-Tolerance Lateral Grinding
A dual-shaft cutting chamber requires exact clearance between counter-rotating knives. Even minor dimensional variations cause lateral binding or premature wear.
| Manufacturing Stage | Machining Technology | Applied Tolerance Standard |
|---|---|---|
| Profile & Hook Milling | 5-Axis CNC Machining Centers | ±0.02 mm claw contour accuracy |
| Bore Broaching & Wire EDM | CNC Broaching / Wire EDM | Hexagonal, keyed, and splined bores to fit exact shaft specs |
| Parallel Face Grinding | Double-Disc CNC Surface Grinders | ±0.005 mm to ±0.01 mm thickness tolerance |
| Edge Sharpening | Precision Tool & Cutter Grinders | Sharp or radiused cutting edges to match material density |
Strict Quality Control and Non-Destructive Testing
Every production batch undergoes a rigid quality protocol before dispatch:
Ultrasonic Flaw Detection: 100% testing of raw forgings to eliminate internal voids, inclusions, and structural cracks.
Coordinate Measuring Machine (CMM): Full 3D inspection verifying hook geometry, bore concentricity, and axial parallelism.
Digital Hardness Testing: Multi-point Rockwell (HRC) testing across the cutting tip, body, and bore contact surfaces.
Hook Profiles and Cutting Dynamics
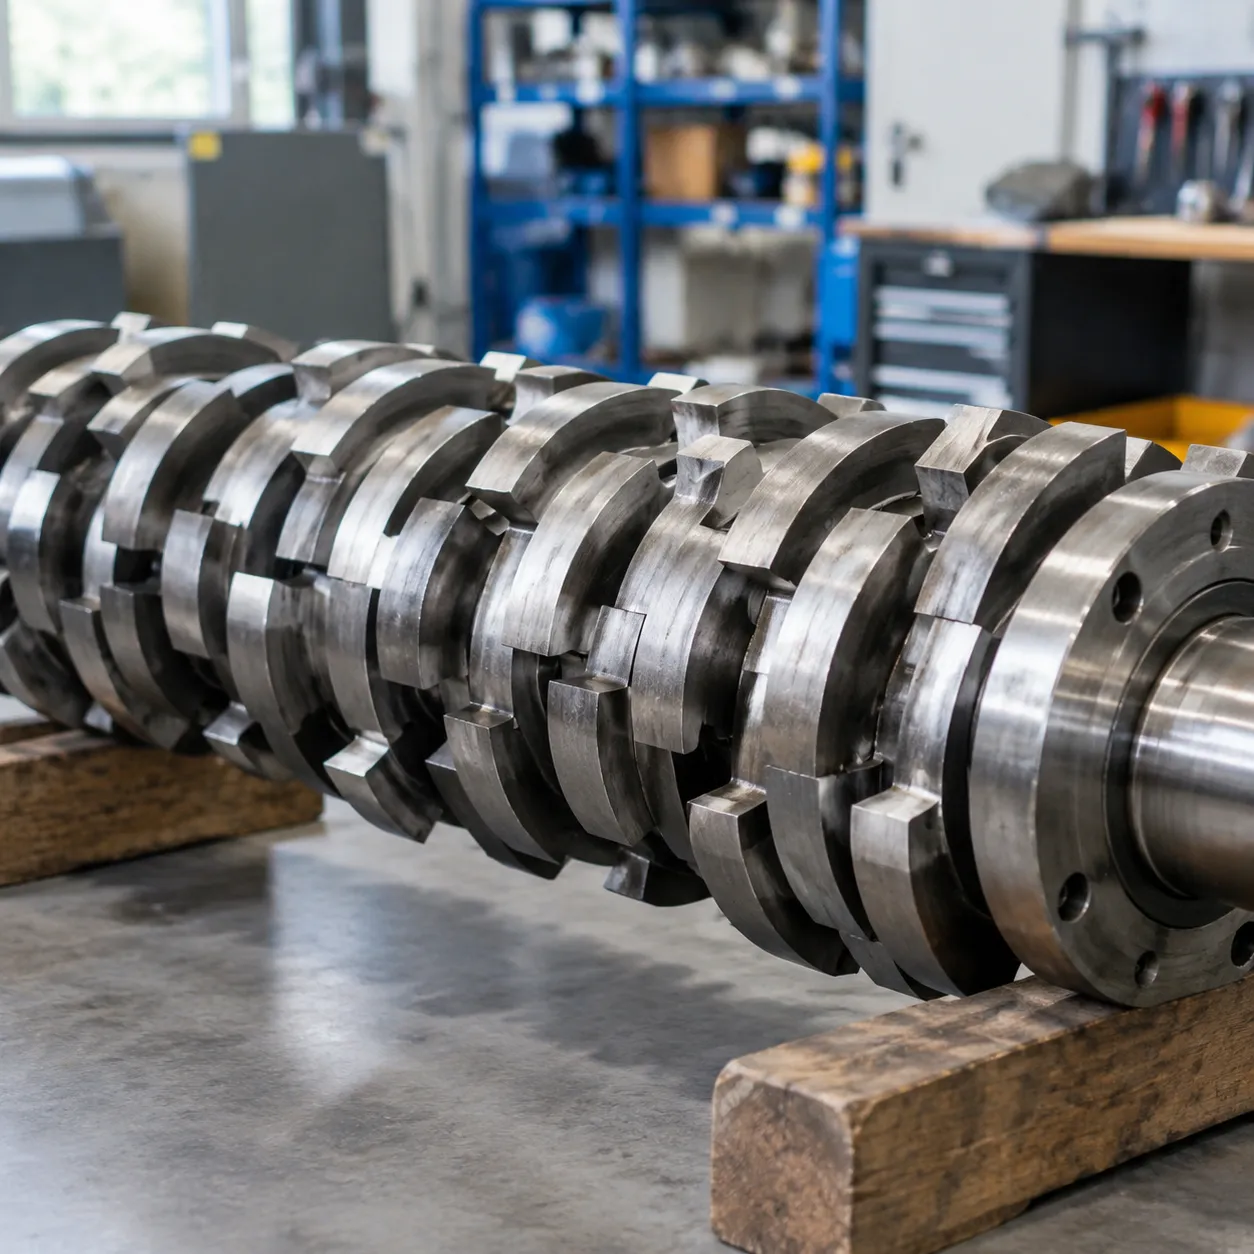
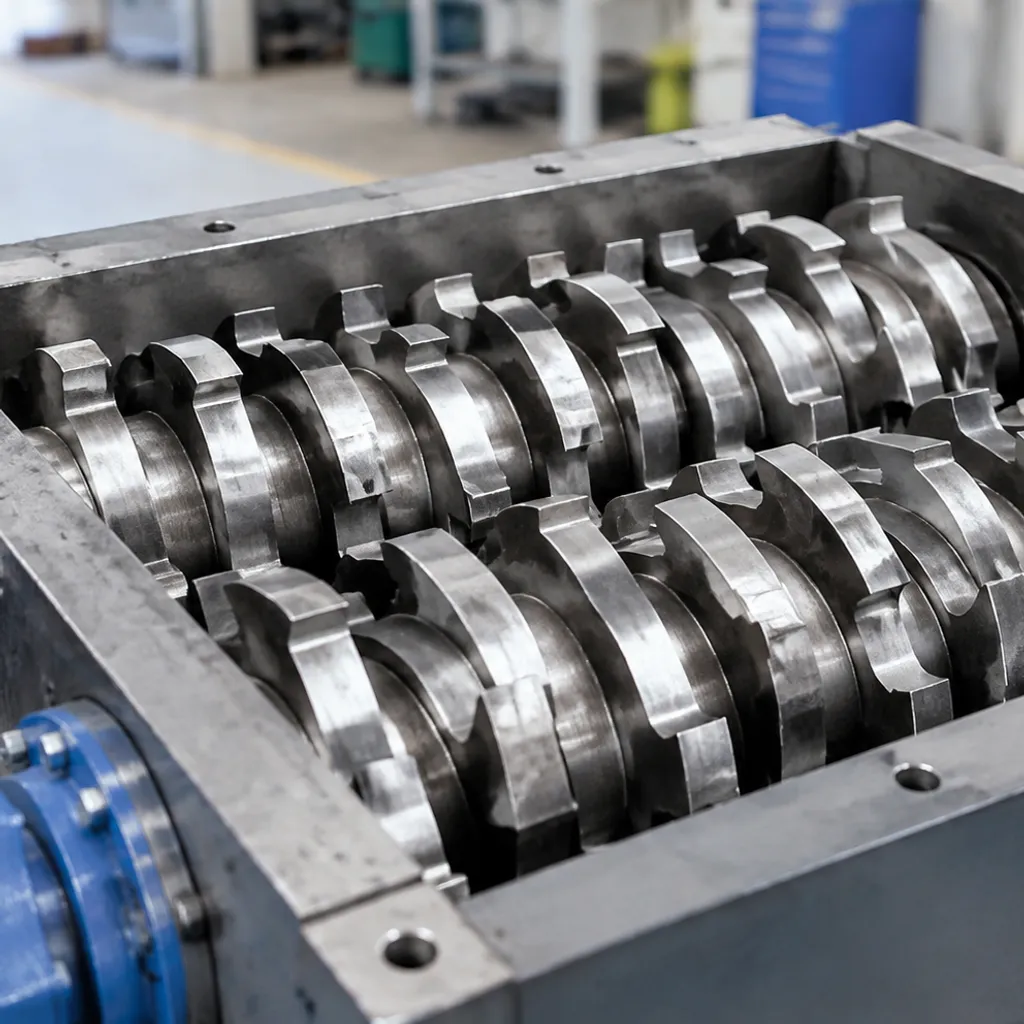
The tooth geometry of double shaft shredder blades dictates intake aggression, rotor torque distribution, and final particle size. We engineer custom hook profiles to match the specific tearing and shearing demands of your material stream:
Single-Claw Blades for Aggressive Intake
Single-hook type shredder cutters concentrate the drive shaft's full rotational torque onto a single point of contact. This focused force delivers maximum penetration, making them essential for grabbing and ripping bulky, hollow, or thick-walled items that resist standard cutting edges.
Primary Applications: Whole passenger and truck tires, steel drums, IBC totes, large plastic purges, and bulky timber pallets.
Cutting Action: High-torque piercing, rapid intake draw, and deep ripping without slippage.
Double and Triple-Claw Knives for Balanced Throughput
Double and triple-claw twin shaft shredder blades distribute cutting forces across multiple points per rotation. This configuration balances continuous material intake with uniform particle reduction, reducing cyclic shock loads on machine gearboxes and electric motors.
Primary Applications: E-waste (WEEE), computer chassis, rigid plastic containers (HDPE/PP), aluminum scrap, and municipal solid waste (MSW).
Cutting Action: Balanced progressive shearing with high throughput and consistent shred size.
Multi-Tooth Discs for High-Frequency Shearing
Multi-tooth dual shaft shredder knives feature multiple smaller hooks around the blade perimeter. This design creates a scissor-like shearing frequency that prevents thin, flexible, or high-tensile materials from wrapping around the rotor shafts.
Primary Applications: Agricultural plastic films, woven jumbo bags (FIBC), packaging wraps, textile waste, and sheet rubber.
Cutting Action: High-frequency, clean edge shearing to eliminate rotor wrapping and reduce fines.
| Claw Configuration | Penetration Force | Shearing Frequency | Target Waste Stream |
|---|---|---|---|
| Single-Claw | Maximum | Low (1 cut/rev) | Bulky, hollow, or heavy-gauge scrap |
| Double-Claw | High | Moderate (2 cuts/rev) | Rigid plastics, electronic scrap, light metals |
| Triple-Claw | Moderate | High (3 cuts/rev) | MSW, mixed commercial waste, rubber parts |
| Multi-Tooth (4+ Claws) | Distributed | Maximum (Continuous) | Films, fibrous materials, textiles, thin sheeting |
Industrial Applications and Processed Waste Streams
Plastics Recycling: Rigid Purges, Containers, and Films
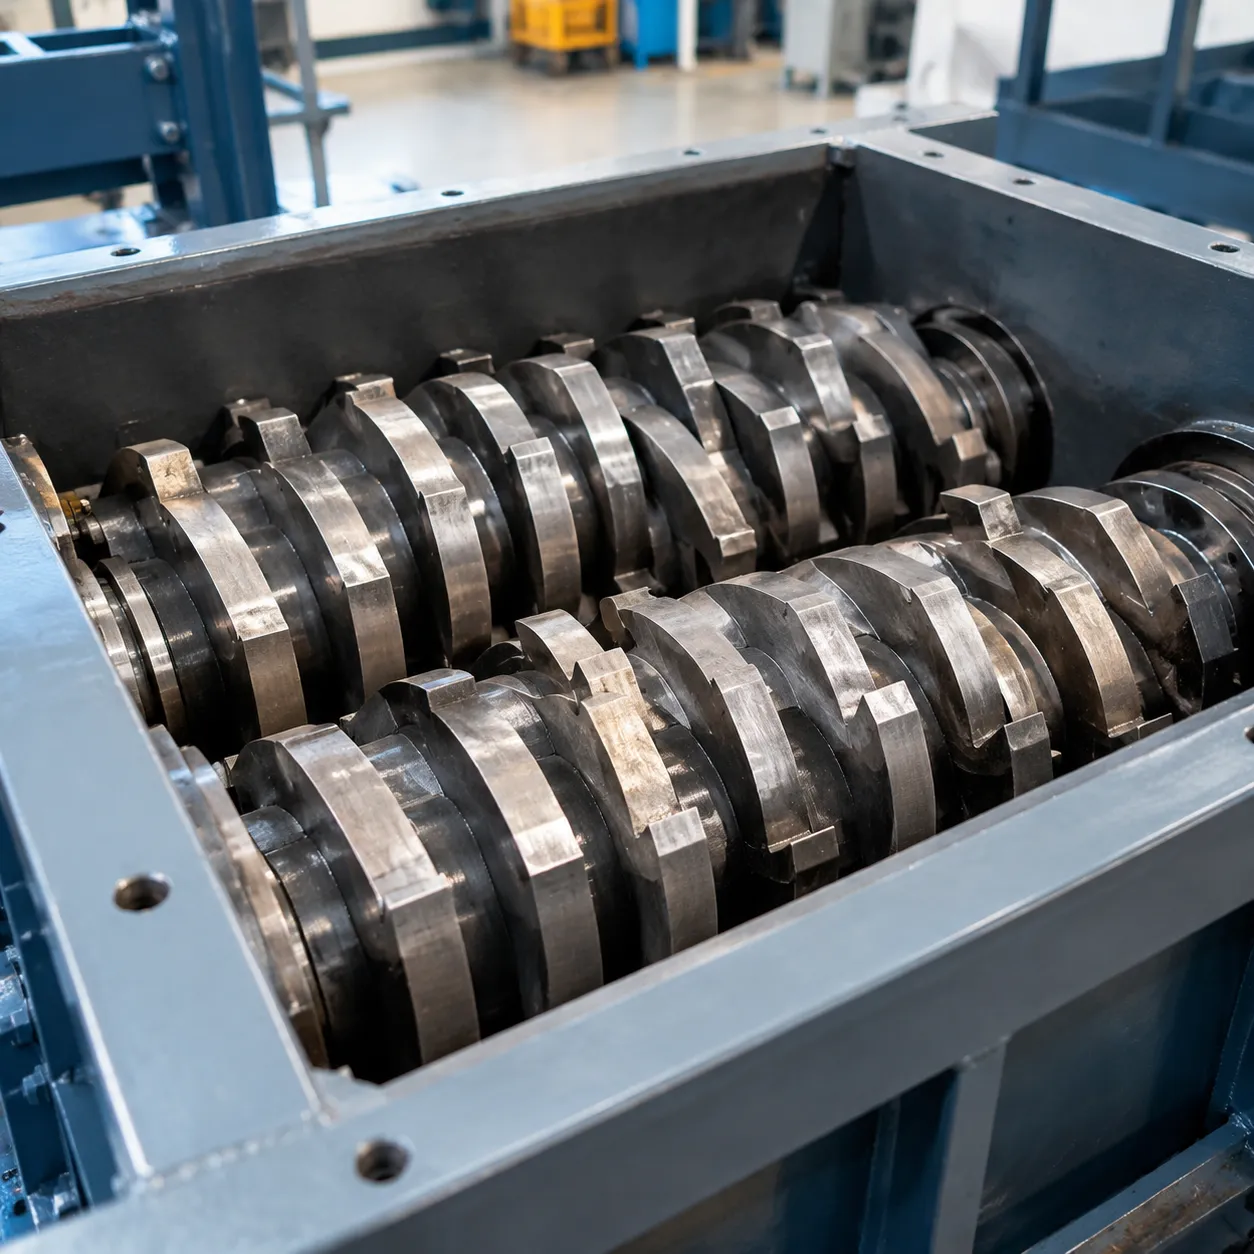
Processing plastics demands sharp cutting edges and high abrasion resistance to prevent polymer melting and edge rounding.
Target Materials: Thick-walled purge lumps, injection molded scrap, blow-molded HDPE drums, PET bottles, agricultural film, and woven PP bulk bags.
Blade Metallurgy: High-carbon, high-chromium tool steels like D2 (1.2379) and DC53 vacuum hardened to 58–62 HRC.
Operational Benefit: Clean, scissor-action shearing that generates clean flakes with minimal fines and prevents stretchable films from wrapping around the rotor shaft.
End-of-Life Tires (ELT) and Rubber Size Reduction
Tire shredding subjects blades to extreme tensile shock and severe metal-on-metal friction from embedded steel beads and radial belts.
Target Materials: Passenger car tires, commercial truck radials, OTR tire sections, and vulcanized rubber treads.
Blade Metallurgy: Shock-resistant alloy steels such as 55SiCr, 6CrW2Si, or 42CrMo tempered to 54–58 HRC to deliver exceptional fracture toughness.
Operational Benefit: Seamless integration with standard systems optimized for demanding rubber processing, keeping hook profiles intact despite continuous high-impact contact with bead wire.
E-Waste and Light Industrial Scrap Metal
Shredding light scrap and electronic scrap requires rigid, high-yield cutter profiles that resist micro-chipping caused by non-ferrous metals and fiberglass.
Target Materials: Printed circuit boards (WEEE), electronic housings, white goods, aluminum extrusions, tin cans, and light sheet metal stampings.
Blade Metallurgy: Tough DC53 and shock-modified H13 tool steels designed to withstand uncrushable contaminants.
Operational Benefit: Our twin shaft shredder blades maintain strict shearing tolerances to cleanly cut through metal sheets without edge roll-over or shaft deflection.
Wood Pallets, Biomass, and Forestry Timber
Reclaiming timber involves handling bulky dimensions and abrasive contaminants such as dirt, stones, and steel fasteners.
Target Materials: Heavy-duty logistics pallets, shipping crates, demolition wood, green waste, and forestry residues.
Blade Metallurgy: Hardened alloy steels engineered to resist notched impact damage from embedded nails, staples, and screws.
Operational Benefit: Aggressive hook angles ensure high-intake feeding for bulky items, pulling logs and pallets directly into the cutting chamber without bridging.
Municipal Solid Waste (MSW) and Hazardous Waste
Mixed waste streams are unpredictable and contain a wide range of abrasive, dense, and corrosive materials.
Target Materials: Mixed household refuse, bulky commercial waste, mattresses, industrial packaging, and steel drums.
Blade Metallurgy: Heavy-duty dual shaft shredder knives utilizing wear-resistant overlays and tough core metallurgy to handle uncrushables.
Operational Benefit: Balanced tearing and shearing forces that shred high volumes reliably while minimizing unplanned plant downtime.
Complete Twin-Shaft Rotor Assemblies and Wear Parts
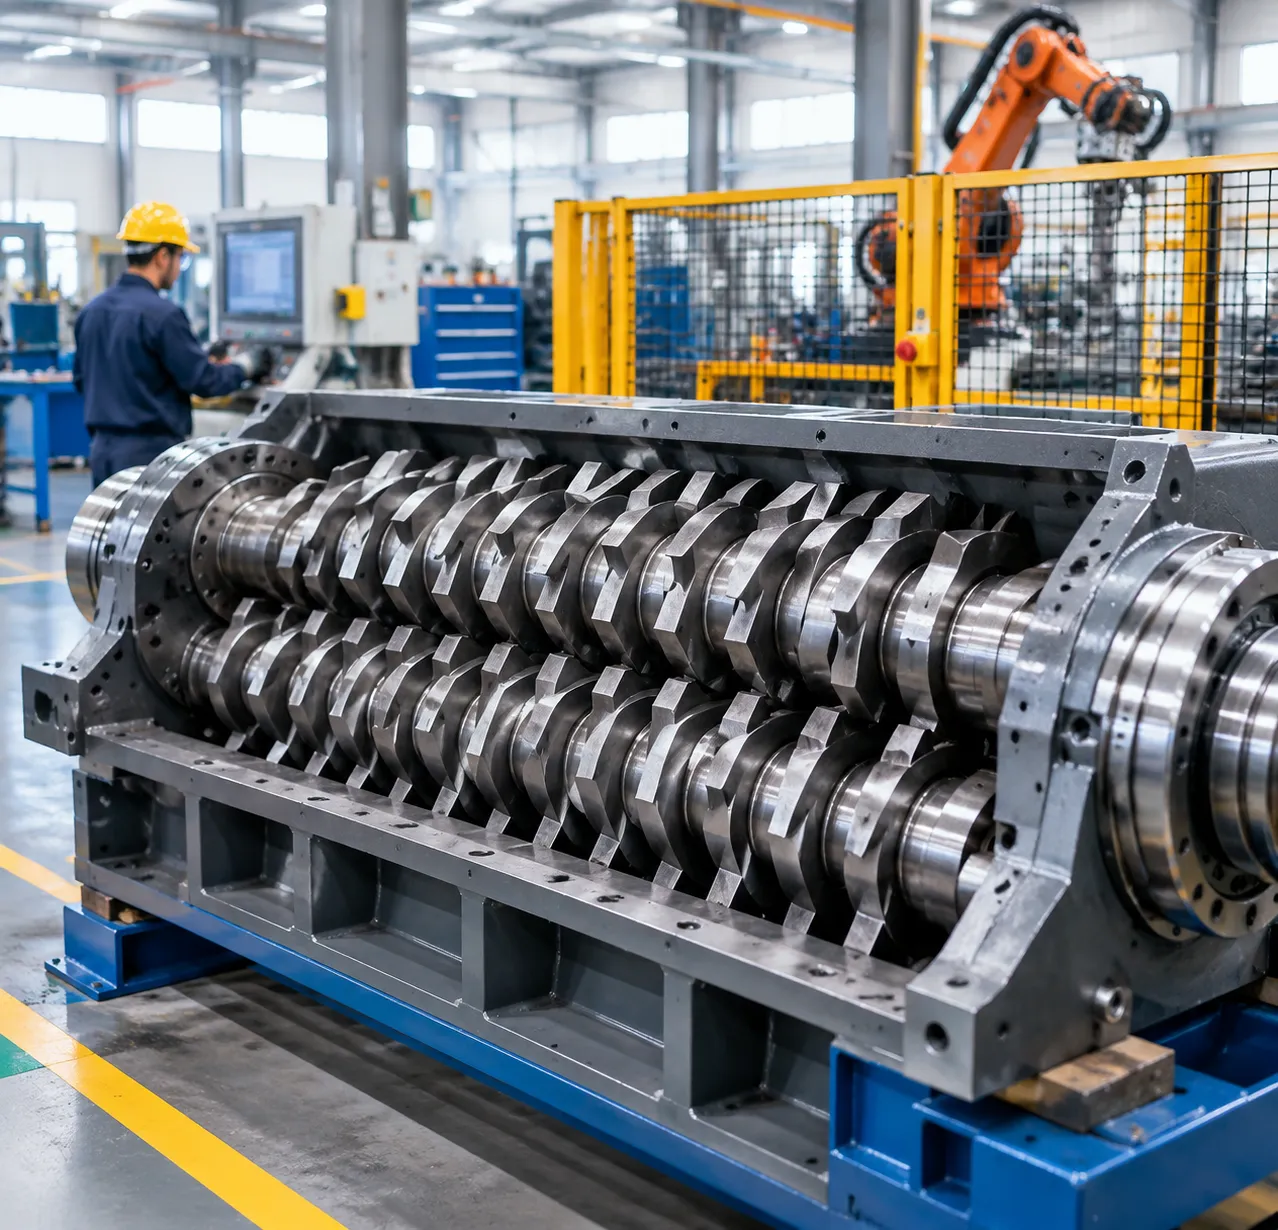
A high-performance cutting chamber relies on the entire cutting system working in sync, not just the blades. We engineer and supply complete rotor assemblies and matching industrial shredder wear parts to eliminate shaft deflection, prevent material wrapping, and maintain exact cutting clearances across heavy-duty reduction cycles.
Hardened Spacers for Axial Clearance Control
Maintaining precise lateral spacing between double shaft shredder blades prevents catastrophic blade-to-blade contact and excessive friction.
Precision Surface Grinding: Ground to tight thickness tolerances (down to ±0.005 mm) to ensure uniform axial stacking without cumulative tolerance stack-up.
Matched Hardness: Manufactured from hardened tool steels and alloy grades to prevent face galling and wear under continuous side-load pressure.
Custom Sizing: Configured to match required blade thicknesses and target output chip sizes.
Wear-Resistant Cleaning Fingers and Scraper Knives
Cleaning fingers (stator scrapers) strip shredded material out from between rotating dual shaft shredder knives, preventing bridging and chamber packing.
Anti-Wrapping Geometry: Profiles tailored to eject stringy plastics, film, tires, and bulky waste before material winds around the shaft.
Heavy-Duty Wear Alloys: Machined from abrasion-resistant steels such as Hardox, D2, and Cr12MoV to endure severe abrasive friction.
Rotor Protection: Proper scraper clearance reduces parasitic motor drag and shields drive components from jamming forces. You can learn more about rotor cutting dynamics in our single shaft vs double shaft shredder blades guide.
Heavy-Duty Forged Hexagonal and Splined Driveshafts
Our drive shafts are engineered to withstand continuous high-torque shearing, sudden shock impacts, and rapid auto-reversing cycles.
High-Strength Forged Alloys: Manufactured from heat-treated alloy steels (such as 42CrMo) for superior torsional fatigue strength and core toughness.
Precision Drive Interfaces: CNC-machined to standard and custom hexagonal, splined, or keyed profiles for a seamless fit with our hexagonal bore shredder blades.
Zero Rotational Play: Tight fitment eliminates drive slippage, shaft rounding, and keyway shearing during extreme uncrushable jams.
Quality Control, Tolerances, and OEM Compatibility
Direct-Fit OEM Replacement Cutters
Our twin shaft shredder blades mount directly onto standard factory shafts and custom-engineered rotors. We supply standard and customized OEM industrial knives tailored to your specific rotor geometry:
Bore Configurations: Precision broached hexagonal, keyed round, square, and involute splined bores.
Direct Interchangeability: 100% compatible with standard commercial shredder housings, spacers, and cleaning fingers.
Balanced Mass: Uniform weight per blade prevents dynamic rotor imbalance and premature gearbox wear.
Zero-Interlocking Gap Calibration
Twin-shaft shredding demands exact lateral spacing to prevent blade deflection, friction-induced overheating, and catastrophic cutter collisions.
- Parallel Surface Grinding: Lateral thickness held within ±0.005 mm to ±0.01 mm for uniform axial compression along the shaft.
- Cutting Edge Alignment: Calibrated hook-to-hook clearance ensures a clean shearing action while preventing material wedging between blade faces.
- Bore-to-OD Concentricity: Strict runout control minimizes radial vibration under severe shredding loads.
Material Traceability and Testing Standards
Every production run undergoes thorough quality control inspection to guarantee performance in high-impact operations:
Raw Steel Verification: Mill Test Certificates (MTC) tracking chemical composition for authentic D2, DC53, and high-impact tool steel grades.
Ultrasonic Flaw Detection: Complete internal scans to identify and eliminate subsurface voids, inclusions, or micro-cracks before machining.
Multi-Point Hardness Verification: Digital Rockwell testing (HRC) across both the cutting claws and the core to verify uniform heat treatment.
Custom Engineering Workflow and RFQ Ordering Guide
We manufacture direct-fit replacement double shaft shredder blades and custom cutting assemblies engineered around your specific rotor layout, scrap material, and throughput targets. Our streamlined Request for Quote (RFQ) process delivers accurate pricing, material recommendations, and manufacturing timelines within 24 hours.
Essential Blade Specifications for Rapid Quotes
To provide an exact quote and tool steel recommendation for your twin shaft shredder blades, we require the core dimensional and operational parameters outlined below:
| Parameter | Required Specification | Typical Engineering Options |
|---|---|---|
| Outer Diameter (OD) | Tip-to-tip cutting diameter | 150 mm to 650+ mm |
| Bore Profile (ID) | Rotor shaft mounting geometry | Hexagonal, Double-Keyed, Splined, Square |
| Blade Thickness (T) | Lateral width across ground faces | 15 mm to 100 mm (Ground to ±0.01 mm) |
| Hook / Claw Count | Number of cutting tips per disc | Single-claw, double-claw, multi-tooth profiles |
| Target Material | Type of waste processed | Rigid plastics, tires, e-waste, scrap metal, MSW |
| Preferred Steel Grade | Metallurgical requirement | D2 (1.2379), DC53, Cr12MoV, 55SiCr, H13 |
Custom Blade Manufacturing from CAD Drawings or Physical Samples
Whether you have original machine blueprints or need to replace obsolete cutters, our team supports full end-to-end fabrication through dedicated custom engineering capabilities:
- Digital CAD File Support: Submit 2D drawings (DWG, DXF, PDF) or 3D solid models (STEP, IGES) for direct integration into our multi-axis CNC milling and Wire EDM centers.
- Reverse Engineering from Worn Samples: Ship your worn dual shaft shredder knives directly to our facility. We utilize CMM digitizers and metallurgical spectrographic testing to recreate exact hook geometries, shaft fits, and alloy compositions.
- Rotor Assembly Matching: We manufacture matched sets of blades, hardened spacers, and cleaning fingers simultaneously to guarantee uniform axial spacing and zero interference across both cutting shafts.
Flexible Production Volumes: Rapid Prototyping to Full Container Loads
Our manufacturing line is configured to support both immediate emergency maintenance runs and regular OEM supply schedules:
- Pilot Runs & Prototype Sets: Low-volume batches for testing new claw geometries, specialized tool steels, or custom wear coatings on problematic waste streams.
- Complete Rotor Re-Tooling Kits: Full replacement packages—including all primary blades, counter knives, wear spacers, and driveshaft hardware—packed and indexed for streamlined installation.
- Volume OEM Supply: Scheduled container-load production contracts with dedicated safety stock programs, batch mill test certificates, and factory-direct pricing.
Frequently Asked Questions: Double Shaft Shredder Blades
How do I choose between D2 and DC53 for double shaft shredder blades?
Material selection depends strictly on the abrasiveness and impact level of your processed waste stream:
| Feature | D2 (1.2379 / SKD-11) | DC53 (Upgraded D2) |
|---|---|---|
| Primary Strength | High wear resistance & edge retention | Exceptional impact toughness (nearly 2x D2) |
| Typical Hardness | 58–62 HRC | 56–60 HRC |
| Best Used For | Rigid plastics, packaging, film, light e-waste | Car tires, heavy scrap metal, dense timber |
| Failure Risk | Prone to micro-chipping under high shock | Slightly lower abrasion resistance in sandy waste |
What causes twin shaft shredder blades to chip, and how can it be prevented?
Blade chipping typically occurs due to three factors:
Unshreddable Contaminants: Tramp metal or oversized rigid inclusions exceeding yield strength.
Axial Play & Misalignment: Worn shredder spacers allow lateral blade deflection, causing cutting edges to collide.
Improper Metallurgy: Over-hardened steel lacking sufficient core toughness.
We prevent edge chipping through proprietary vacuum heat treatment and triple tempering. For high-impact size reduction, we calibrate blade hardness down to 54–58 HRC using shock-resistant alloy steels like DC53 or 6CrW2Si.
Can replacement shredder blades be manufactured from a worn sample?
Yes. If original CAD blueprints are unavailable, our engineers reverse-engineer your dual shaft shredder knives directly from physical samples:
CMM Coordinate Measurement: Reconstructs exact hook profiles, outer diameters, and bore dimensions.
Optical Spectrum Analysis: Identifies base steel composition to match or upgrade the alloy grade.
Worn Edge Compensation: Restores original cutting clearances to ensure compatibility with our full line of industrial recycling blades and drive components.
What is the standard production lead time for custom shredder knives?
Standard production for custom double shaft shredder replacement cutters ranges from 3 to 5 weeks, depending on tool steel availability, bore geometry complexity, and order volume. Expedited manufacturing schedules are available for critical maintenance shutdowns and emergency replacements.
How do blade thickness and hook count affect motor load and particle size?
Blade geometry directly dictates cutting dynamics and drive torque demand:
- Blade Thickness (Width): Dictates final shred strip width. Thinner blades create narrower shred strips but increase the total number of cutters on the rotor, raising the required drive torque. Thicker blades resist bending under extreme shock loads.
- Hook Count:
- Single-claw: Delivers maximum penetration and aggressive pull-in for bulky, hollow items (drums, tires) with lower motor drag.
- Multi-claw: Delivers higher cutting frequency per shaft rotation, generating smaller and more uniform output chips while requiring higher steady-state torque.