Formula details
Product Details
Overview
What Is a Coil Slitter Knife and How Does It Work?
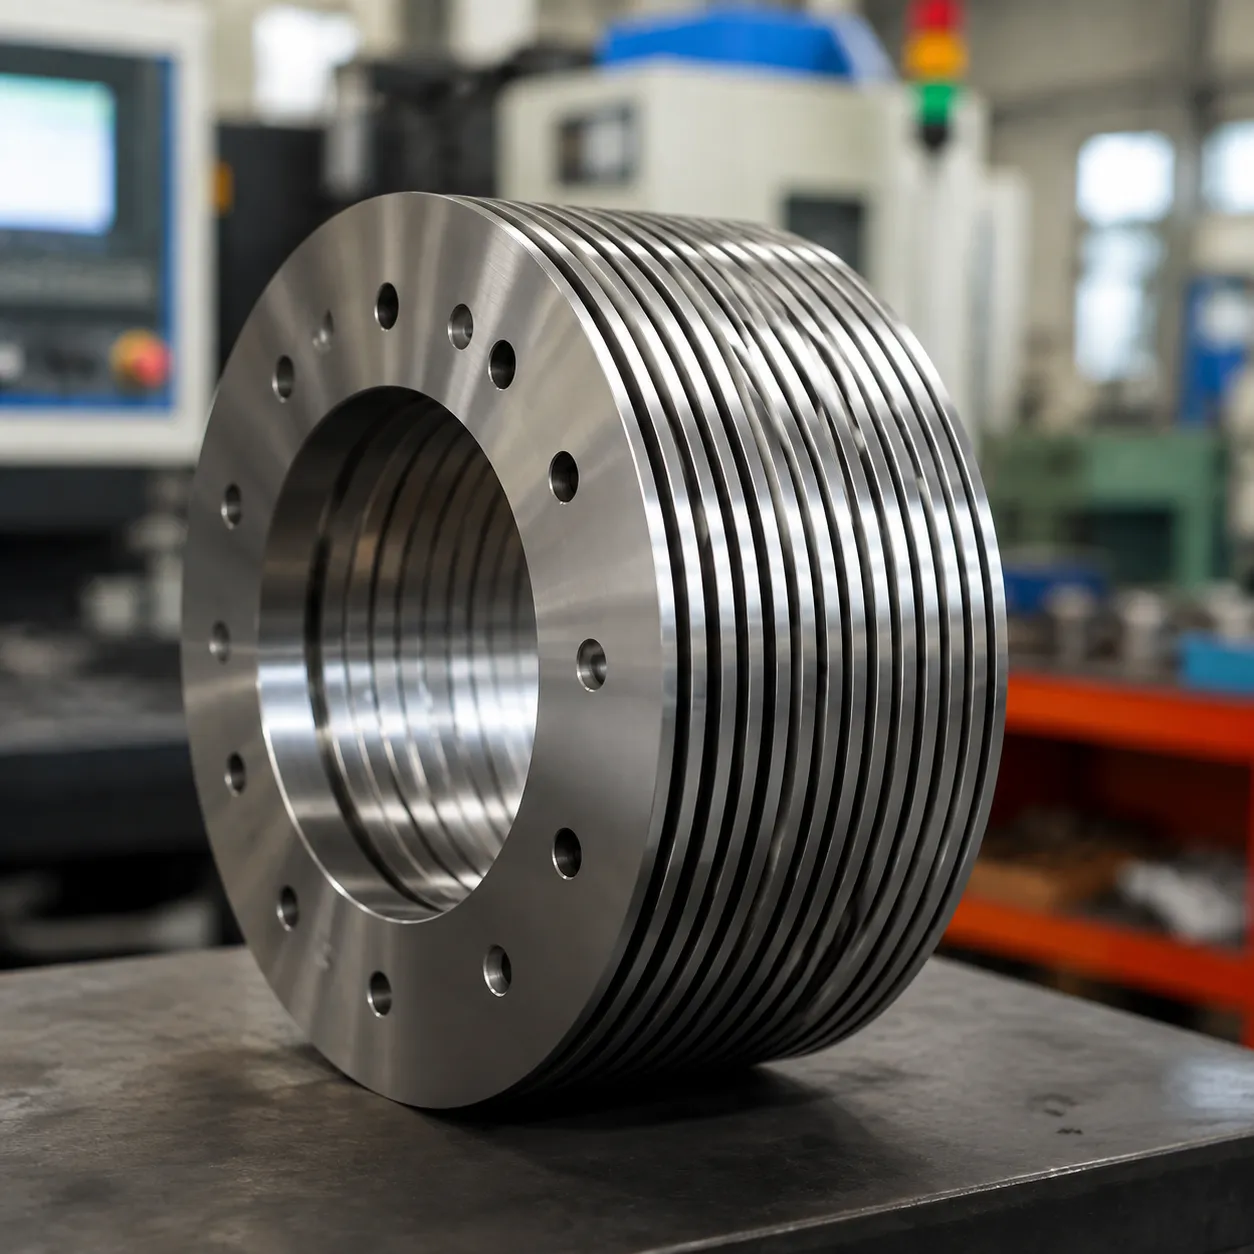
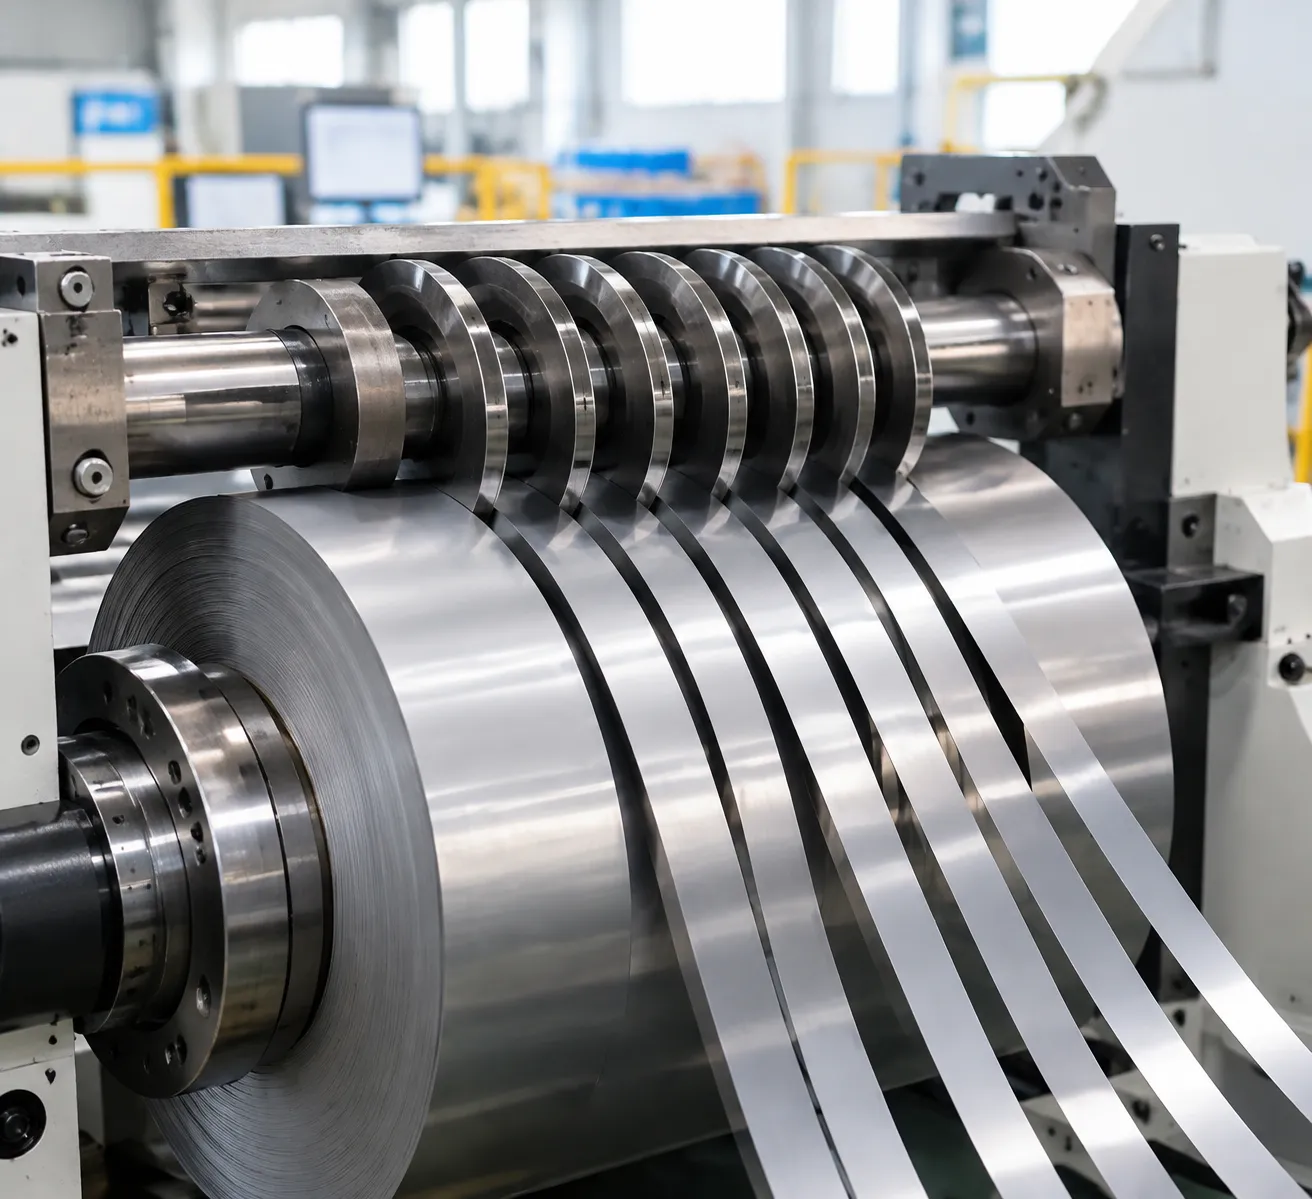
A coil slitter knife is a high-precision, circular cutting tool mounted on rotating arbors to slice wide master coils of sheet metal into narrower strips. Rather than chopping through material like a guillotine blade, a coil slitting knife relies on rotary shear dynamics.
In metal processing lines, our rotary slitter blades operate in opposing pairs—top and bottom—to deliver continuous, high-speed longitudinal cuts through carbon steel, stainless steel, aluminum, and advanced high-strength steels (AHSS).
[ Top Arbor ] ---> [ Top Knife ]
==> [ Metal Strip Fractures Cleanly ]
[ Bottom Arbor ] ---> [ Bottom Knife ] /
Core Working Principles of Rotary Coil Slitting
Rotary coil slitting is not a simple cutting action; it is a synchronized process of controlled deformation, localized penetration, and precise material fracture.
- The Penetration Stage (Shear Zone): As the metal strip passes between the overlapping top and bottom knives, the cutting edges penetrate the top and bottom surfaces of the metal. This forms the clean, vertical depth of penetration (typically 15% to 35% of total strip thickness, depending on tensile strength).
- The Fracture Stage (Break Zone): Once the shear stress exceeds the ultimate shear strength of the coil, micro-cracks form and propagate between the opposing knife edges. The remaining material fractures cleanly along this shear plane.
- Burr-Free Separation: Precise alignment prevents tearing, yielding an edge with minimal burr, a straight burnish zone, and zero edge camber.
Key Setup Components of the Slitter Tooling Arbor
A knife cannot perform in isolation. Achieving tight width tolerances and clean slit edges requires a balanced assembly across the slitting machine arbor:
- Top and Bottom Slitter Knives: The primary cutting elements ground to mirror finishes with ultra-tight thickness tolerances to maintain dimensional stability under high lateral loads.
- Slitter Tooling Spacers: Precision-ground steel or lightweight alloy rings placed between knives to determine the exact slit width of the finished coils.
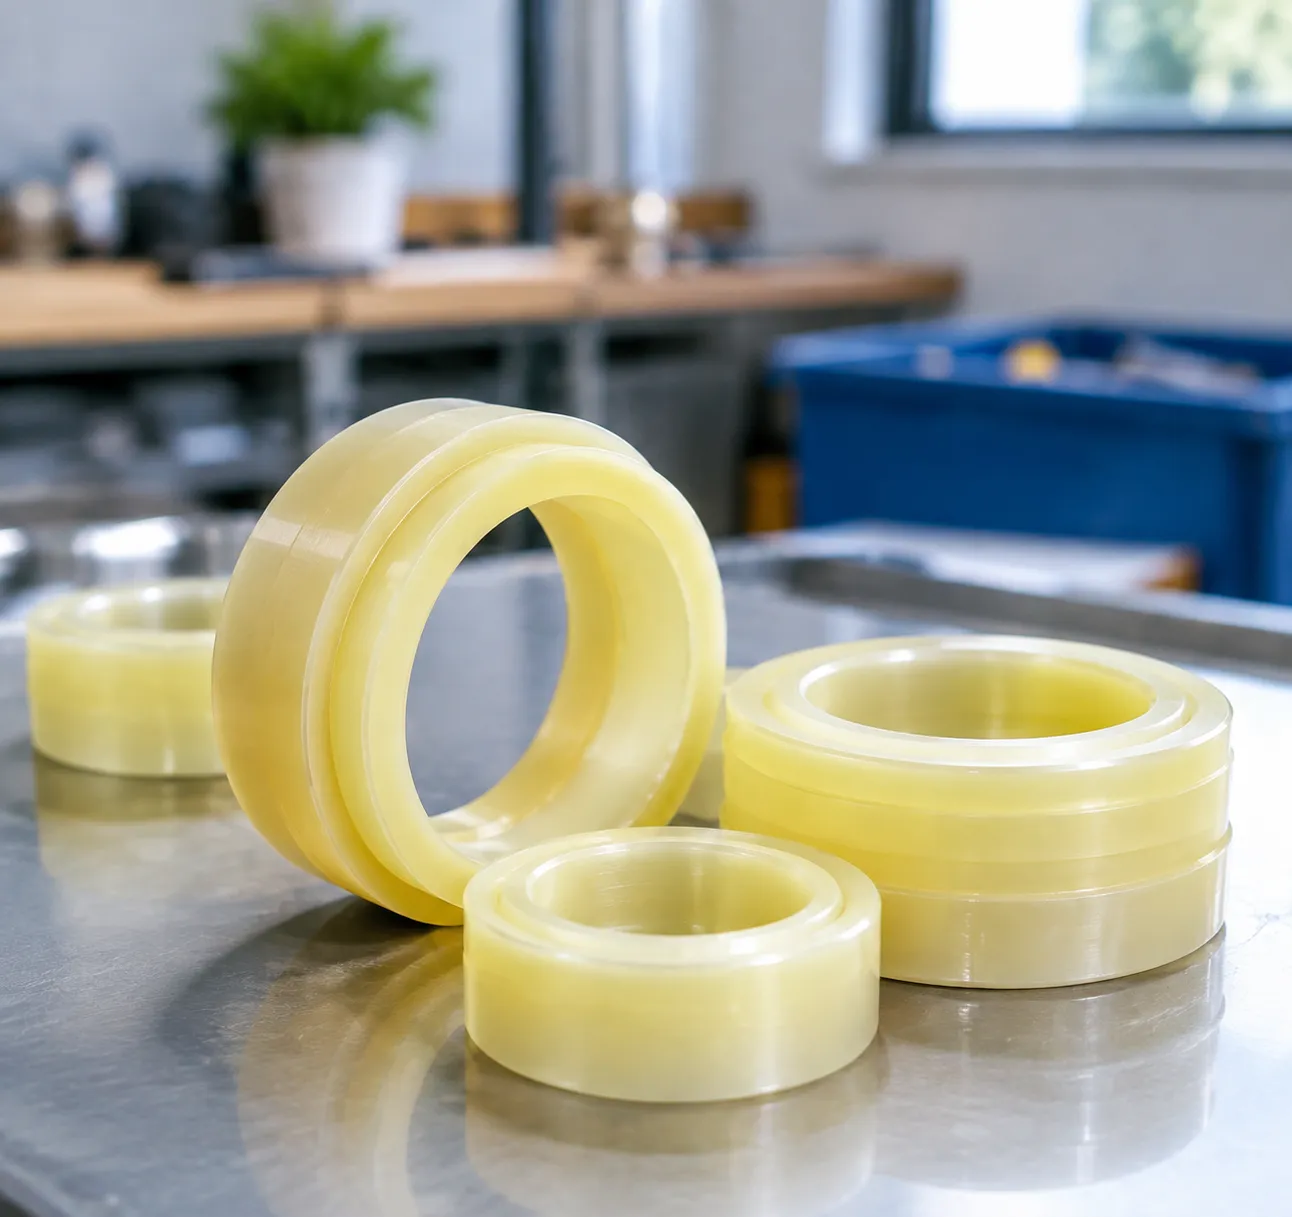
- Polyurethane Stripper Rings: Mounted alongside the knives to support the strip during cutting and actively push the slit strands off the blade faces, preventing strip jamming, edge wave, and scuffing.
- Locking Nuts and Arbors: The mechanical foundation that secures the tooling pack under heavy axial compression to prevent axial deflection or knife wobble.
Precision Coil Slitter Knives vs. Standard Rotary Shear Blades
While standard rotary shear blades handle general shearing, scrap cutting, or rough trimming, precision coil slitter knives must meet extreme geometric tolerances to prevent edge burrs and strip-width variation.
| Feature / Specification | Standard Rotary Shear Blades | Precision Coil Slitter Knives |
|---|---|---|
| Thickness Tolerance | ±0.005 mm to ±0.010 mm | ±0.001 mm (±0.00004 in) |
| Parallelism & Flatness | ≤ 0.005 mm | ≤ 0.002 mm |
| Surface Finish (Ra) | 0.4 µm to 0.8 µm | 0.1 µm to 0.2 µm (Mirror Finish) |
| Primary Failure Risk | Blade wear, chipping | Lateral deflection, slit edge burrs |
| Typical Target Materials | Plate shearing, scrap, structural metal | AHSS, silicon steel, thin foil, cold rolled coils |
| Tooling Configuration | Shim-dependent, manual setups | High-precision shimless slitting assemblies |
Practical Line Tips for Extended Tool Life
- Maintain Zero Radial Runout: Even a 0.003 mm runout on an arbor creates uneven knife penetration, producing intermittent burrs on one side of your slit strand.
- Clean Tooling Faces Every Setup: Grease, micro-chips, or grit between a knife and a spacer multiply axial runout across the arbor. Always wipe knife and spacer contact faces completely clean before locking the assembly.
Tool Steels and Carbide Materials for Slitter Knives
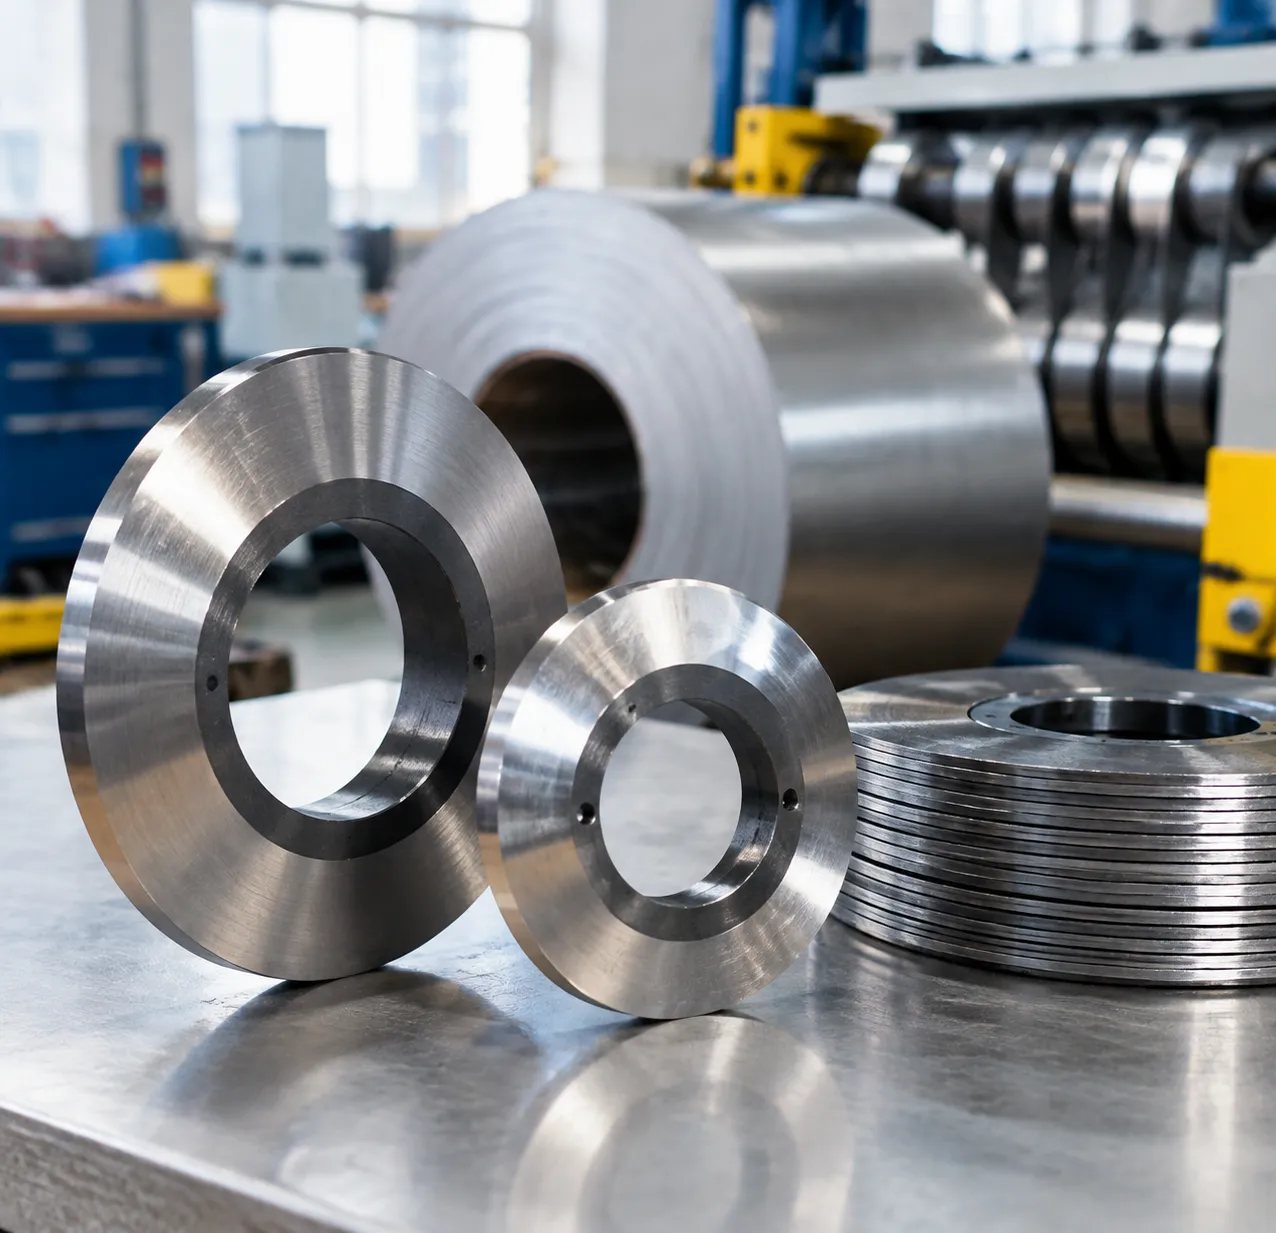
Choosing the right alloy for your coil slitter knife directly controls your run time between sharpenings, edge burr levels, and tooling life. We balance hardness, wear resistance, and impact toughness to prevent edge chipping when running tough alloys at high arbor speeds. For a detailed breakdown of metallurgical grades, reference our comprehensive slitter blade material guide.
D2 High-Carbon High-Chromium Tool Steel
D2 is our baseline workhorse material for processing standard sheet metal and light-to-medium gauge strips.
Core Strengths: Deep-hardening properties, high compressive strength, and balanced wear resistance.
Best Applications: Low-carbon steel, galvanized coil, tinplate, and general fabrication slitting lines.
Hardness Range: 58–62 HRC.
M2 High-Speed Steel (HSS)
When arbor friction and strip speeds increase, standard tool steels soften at the cutting edge. We deploy M2 high-speed steel to maintain red-hardness under continuous, high-volume production.
Core Strengths: Superior abrasion resistance and thermal stability due to high tungsten, molybdenum, and vanadium alloying.
Best Applications: Medium-to-heavy gauge cold-rolled steel, pickling lines, and high-speed coil slitting tooling setups.
Hardness Range: 62–64 HRC.
Tungsten Carbide and Carbide-Tipped Knives
For abrasive, work-hardening, or ultra-hard metal strips, solid or inlaid tungsten carbide slitter blades outperform conventional steels by holding an edge significantly longer. To evaluate whether the extended run-time justifies the initial investment on your arbor, examine our carbide vs steel knives guide.
Core Strengths: Extreme hardness, zero edge deflection, and resistance to severe abrasive wear.
Best Applications: Silicon electrical steels, spring steel, thin-gauge foils, and high-tensile materials.
Hardness Range: 88–92 HRA.
Material Selection Guide for Metal Coils
| Coil Material | Recommended Blade Grade | Typical Hardness | Primary Operational Benefit |
|---|---|---|---|
| Carbon Steel (CRS/HRS) | D2 / High-Cr Alloy | 58–60 HRC | Resists edge roll under standard coil tension |
| Stainless Steel (300/400 Series) | M2 HSS or Powder Metal | 62–64 HRC | Prevents edge galling and withstands work-hardening |
| Silicon Electrical Steel | Tungsten Carbide | 89–91 HRA | Eliminates burrs across millions of cuts |
| Aluminum & Copper Alloys | Cryogenic D2 / High-Purity HSS | 60–62 HRC | Minimizes material pickup and keeps slit edges clean |
Critical Precision Tolerances and Technical Specifications for Coil Slitter Knives
When dealing with high-speed slitting, blade dimensional accuracy directly dictates edge quality, burr formation, and overall arbor stability.
OD, ID, and Thickness Tolerances
Maintaining exact thickness and bore accuracy prevents cumulative stack-up errors and eliminates arbor play during heavy-duty slitting operations.
| Parameter | Standard Precision Tolerance | Ultra-Precision / Shimless Tolerance |
|---|---|---|
| Thickness (T) | ±0.002 mm (±0.00008") | ±0.0005 mm (±0.00002") |
| Bore Diameter (ID) | +0.010 / +0.020 mm | +0.005 / +0.010 mm |
| Outer Diameter (OD) | ±0.025 mm (±0.001") | ±0.010 mm (±0.0004") |
| Parallelism & Flatness | Within 0.002 mm | Within 0.001 mm |
Flatness, Parallelism, and Surface Finish
Even minor face runout or thickness variations cause knife wobble, leading to inconsistent horizontal clearance and jagged slit edges.
- Parallelism and Flatness: Both blade faces must be strictly parallel within 0.001 mm to 0.002 mm. This tight tolerance stops side deflection when tooling packs are clamped on the arbor.
- Ground vs. Mirror Finish: Standard ground finishes (Ra 0.2–0.4 µm) provide reliable performance on carbon steel lines. For sensitive materials like aluminum, copper, and bright-finish stainless steel, we utilize specialized precision machining techniques to produce a mirror lapped finish (Ra ≤ 0.05 µm). This eliminates microscopic grind marks, reducing strip friction and preventing pickup or material galling.
Hardness Requirements (HRC) and Cryogenic Heat Treatment
Achieving the right balance between wear resistance and edge toughness requires specialized thermal processing:
- Hardness Optimization: Our D2 and high-speed steel rotary slitter blades are hardened to 58–64 HRC depending on strip thickness, while tungsten carbide slitter knives operate at 88–92 HRA for maximum edge life.
- Deep Cryogenic Treatment: Sub-zero cryogenic stabilization transforms retained austenite into tempered martensite. This advanced heat treatment relieves internal micro-stresses, stops blade dimensional drift over time, and delivers up to a 40% increase in wear resistance during continuous slitting cycles.
Knife Clearance and Vertical Overlap Setup Guide
Getting a clean, burr-free cut from your coil slitter knife tooling comes down to two critical setup parameters: horizontal clearance and vertical overlap. When your arbors are properly aligned and dialed in, you maximize tool life and achieve consistent edge quality across the entire coil width.
Calculating Horizontal Clearance Based on Coil Thickness and Tensile Strength
Horizontal clearance—the side-to-side gap between the upper and lower rotary slitter blades—controls how the metal fractures during slitting. We calculate horizontal clearance as a direct percentage of the metal strip thickness, factoring in the tensile strength of the incoming material:
- Soft Aluminum & Copper (Low Tensile): 6% to 8% of strip thickness.
- Mild Carbon Steel (Standard Tensile): 8% to 10% of strip thickness.
- Stainless Steel & High-Strength Steels (AHSS): 10% to 14% of strip thickness.
Setting clearance too tight accelerates knife edge wear and increases motor load on your slitting line arbor. Setting it too loose causes rollover and heavy burrs. Understanding how rotary knife cutters work in metal slitting helps your operators balance shear penetration and clean edge fracture.
| Material Type | Tensile Strength Range | Recommended Clearance (% of Thickness) |
|---|---|---|
| Aluminum Alloys | 100 – 250 MPa | 6% – 8% |
| Cold-Rolled Mild Steel | 270 – 450 MPa | 8% – 10% |
| Austenitic Stainless (304/316) | 500 – 750 MPa | 10% – 12% |
| Advanced High-Strength Steel (AHSS) | 800+ MPa | 12% – 15% |
Adjusting Vertical Overlap (Depth of Cut) for Clean Shearing
Vertical knife overlap dictates how deep the top and bottom slitter knives penetrate the material before the tensile break occurs:
- Thin Gauge Strips (< 0.5 mm): Positive overlap (knives overlap slightly, typically +0.1 mm to +0.3 mm) to ensure full penetration without pulling the web down.
- Medium Gauge (0.5 mm to 2.0 mm): Near-zero to slightly positive overlap to balance cut face depth and knife deflection.
- Heavy Gauge Strips (> 2.0 mm): Negative overlap (a visible vertical gap between knife edges) where strip thickness bridges the gap, initiating shear through high compression.
Rule of Thumb: Penetrate only 20% to 35% of the strip thickness with the blade edge; let the natural tensile stress of the steel complete the remaining 65% to 80% fracture.
Selecting Compatible Polyurethane Stripper Rings to Support Precise Edge Break
Polyurethane stripper rings do more than just eject the cut strands from the arbor—they clamp the strip flat against the knife face during the cut.
- Durometer Selection: Use 70 to 80 Shore A (soft) rings for aluminum and delicate painted coils to prevent surface marking. Choose 85 to 95 Shore A (firm) rings for carbon and stainless steel coils to provide rigid support against edge distortion.
- Outside Diameter (OD) Sizing: Size stripper ring ODs slightly larger than the coil slitter knife OD (typically +1.0 mm to +3.0 mm depending on gauge) to ensure proper material pre-clamping before the shear cut begins.
- Positioning: Pair hard rings adjacent to the knife body to support clean fracture lines, and use softer outer rings to guide and smoothly discharge the slit strands without creating edge wave or twist.
Troubleshooting Common Slitting Defects and Tool Wear
Fixing Edge Burrs, Camber, Twist, and Slit Edge Wave
Most strip defects come down to improper tooling setups, incorrect ring choices, or worn metal coil slitter knives.
| Slitting Defect | Likely Root Cause | Practical Solution |
|---|---|---|
| Excessive Edge Burrs | Excessive horizontal knife clearance or dull blade edges | Tighten horizontal clearance to achieve clean slitted edge burr reduction; replace or sharpen dull knives. |
| Strip Camber & Twist | Asymmetrical clearance or mismatched stripper ring ODs | Match clearance symmetrically across the slitting line arbor and calibrate stripper ring outside diameters. |
| Slit Edge Wave | Excessive vertical knife overlap forcing the metal strip down | Back off vertical overlap so the knives shear only to the material fracture point. |
| Edge Flaking (Double Shear) | Clearance set too tight, causing secondary cutting | Widen horizontal side clearance to let the metal break naturally. |
Identifying Causes of Knife Edge Chipping, Spalling, and Galling
When rotary slitter blades wear out ahead of schedule, their surface wear patterns tell you exactly what went wrong:
- Edge Chipping: Often triggered by blade-to-blade contact during setup, severe arbor deflection, or running high-strength steel without adequate impact toughness. Switching to shock-resistant tool steels or integrating our 150mm precision slitter blade configurations helps absorb heavy impact loads without micro-fracturing.
- Spalling: Surface flaking along the knife face caused by excessive clamping torque, dirty spacers, or foreign debris trapped on the arbor.
- Galling and Material Build-Up: Occurs when soft metals like aluminum or galvanized coatings weld themselves to the knife sidewall under high friction. Maintain mirror-polished side faces and apply consistent lubrication to stop adhesion.
Knife Regrinding Guidelines and Tracking Minimum Usable Blade Diameters
A consistent slitter knife regrinding and sharpening routine protects your tool investment and ensures repeatable cut quality.
- Grind in Matched Sets: Always regrind top and bottom coil slitter knife pairs together so their outside diameters (OD) match within ±0.002 mm.
- Control Grinding Heat: Use wet flood-coolant grinding to prevent localized overheating, which destroys blade hardness and causes surface micro-cracking.
- Track Minimum Blade Diameters: Establish a strict discard limit for outer diameters. Running a coil slitter knife past its minimum allowable diameter forces the arbors closer together, increasing gear wear and causing severe edge distortion.
- Verify Side Parallelism: After sharpening the OD, lightly skim-dress side faces if lateral runout exceeds machine tolerances.
Choosing the Right Slitter Tooling System for Your Line
Matching Blade Grades to Material Types
Different coil metals require specific tool steel alloys and carbide grades to balance impact toughness against abrasive edge wear:
| Coil Material | Recommended Knife Material | Hardness (HRC) | Key Performance Advantage |
|---|---|---|---|
| Mild / Low-Carbon Steel | High-Carbon D2 / Cr12MoV | 58–60 HRC | Excellent balance of cost, toughness, and standard edge life |
| Advanced High-Strength Steel (AHSS) | Modified Shock-Resistant Tool Steel / M2 HSS | 60–62 HRC | High impact resistance to prevent edge spalling and micro-chipping |
| Silicon / Electrical Steel | Premium Tungsten Carbide / Micro-Grain Carbide | 64–68 HRC | Superior wear resistance against highly abrasive, brittle alloys |
| Aluminum & Copper Strip | Precision-Polished D2 or CPM Tool Steels | 59–61 HRC | Mirror-polished side faces prevent material pick-up and galling |
For demanding slit lines, our precision-ground circular slitter knives deliver consistent edge geometry across high-tonnage production runs.
Conventional Shimmed Setups vs. High-Precision Shimless Slitter Tooling
Tooling configurations directly influence setup time and strip accuracy:
- Conventional Shimmed Tooling: Uses standard ground spacers combined with thin plastic or steel shims to dial in horizontal clearance. While cost-effective upfront, it requires skilled operator adjustments and increases the risk of cumulative tolerance stacking.
- Shimless Slitter Tooling Systems: Utilizes computer-optimized, ultra-precise CNC-ground spacers and knives manufactured to ±0.00004" (±0.001 mm) thickness tolerances. This eliminates loose shims, slashes setup time by up to 70%, and ensures repeatable cutting clearances across the entire arbor width.
Custom Tooling Configurations: Light-Gauge vs. Heavy-Gauge Slitting
Optimizing your slitter tooling package requires tailoring the knife geometry and support tooling to the stock thickness:
- Light-Gauge Strip (under 0.020" / 0.5 mm): Requires smaller outer-diameter knives to minimize strip deflection, paired with soft, color-coded polyurethane stripper rings and precision ground spacers to maintain tight clearance without inducing edge camber or waviness.
- Heavy-Gauge Coil (over 0.125" / 3.2 mm): Demands heavy-cross-section knives, robust dual-hardness steel stripper rings, and deep-seated keys on the arbor to handle extreme shear loads and severe shock impacts without blade deflection.
Frequently Asked Questions About Coil Slitter Knives
How often do coil slitter knives need to be resharpened?
Regrinding frequency depends on the processed metal grade, strip thickness, line speed, and blade material. On standard carbon steel lines, a quality D2 or high-speed steel blade can run hundreds of tons before needing service. For abrasive or heavy-gauge jobs, inspect cutting edges regularly. We recommend regrinding as soon as you notice minor edge breakdown or micro-chipping to extend the overall lifespan of your rotary slitting knives and prevent excess arbor load.
What causes excessive burrs during metal coil slitting?
Excessive edge burr typically traces back to four common setup or tooling issues:
Incorrect horizontal clearance: Excessive clearance causes tensile tearing instead of a clean shear; insufficient clearance forces secondary shearing and rapid blade wear.
Dull or chipped knife edges: Rounded cutting edges drag the strip down rather than cleaving it.
Improper vertical overlap: Too much overlap creates high tool friction and burrs; too little causes incomplete fractures.
Arbor runout or poor spacers: Axial play shifts your clearance during operation, leading to inconsistent cut quality across the slit width.
What is the ideal clearance percentage for stainless steel vs. aluminum coils?
Horizontal knife clearance is calculated as a percentage of the total metal thickness:
Stainless Steel: Typically set between 8% and 12% of material thickness. Austenitic grades work-harden rapidly, requiring tight clearances and sharp tooling to shear cleanly before the strip hardens.
Aluminum Alloys: Typically set between 6% and 10% for soft to medium tempers. Harder temper alloys may require up to 12% to avoid pinching and edge rollover.
| Coil Material | Recommended Clearance (% of Thickness) | Primary Concern |
|---|---|---|
| Mild Carbon Steel | 7% – 10% | Balanced shear-to-break ratio |
| Stainless Steel (300/400 series) | 8% – 12% | Rapid work-hardening and edge burr |
| Aluminum (Soft/Medium) | 6% – 10% | Material pickup and galling |
| Copper & Brass | 6% – 8% | Ductility and edge rollover |
Can tungsten carbide slitter knives handle high-strength steels (AHSS)?
Tungsten carbide provides unmatched wear resistance and edge retention on thin-gauge, highly abrasive coils. When slitting advanced high-strength steels (AHSS), shock loads and strip snap-through increase significantly. We engineer specific micro-grain tungsten carbide slitter knife designs with optimized toughness for thin, high-yield applications, while heavy-gauge AHSS processing generally benefits from shock-resistant matrix tool steels.
How do stripper rings impact the cutting quality of rotary slitter knives?
Polyurethane stripper rings do far more than just eject the slit strips from between the blades. They provide essential vertical counter-pressure directly at the shear point:
Prevents strip deformation: Keeps the metal flat against the knife face, stopping edge curl, camber, and edge wave.
Maintains clean fractures: Stabilizes the material during shearing, directly improving cut accuracy and reducing edge burrs.
Protects surface finish: High-grade polyurethane compounds prevent scratching and marking on sensitive materials like prepainted coils, bright-finish stainless steel, and polished aluminum.